Where there's space - there's possibility

Leave Your Message
Where there's space - there's possibility
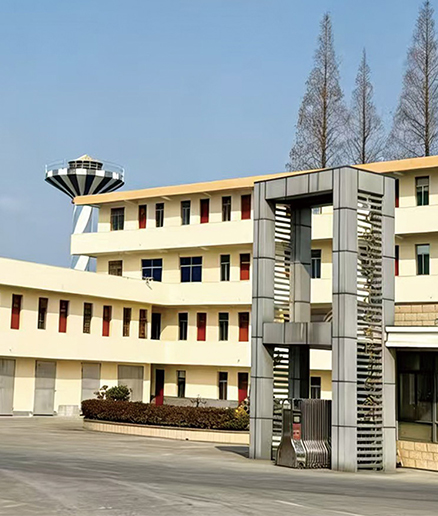
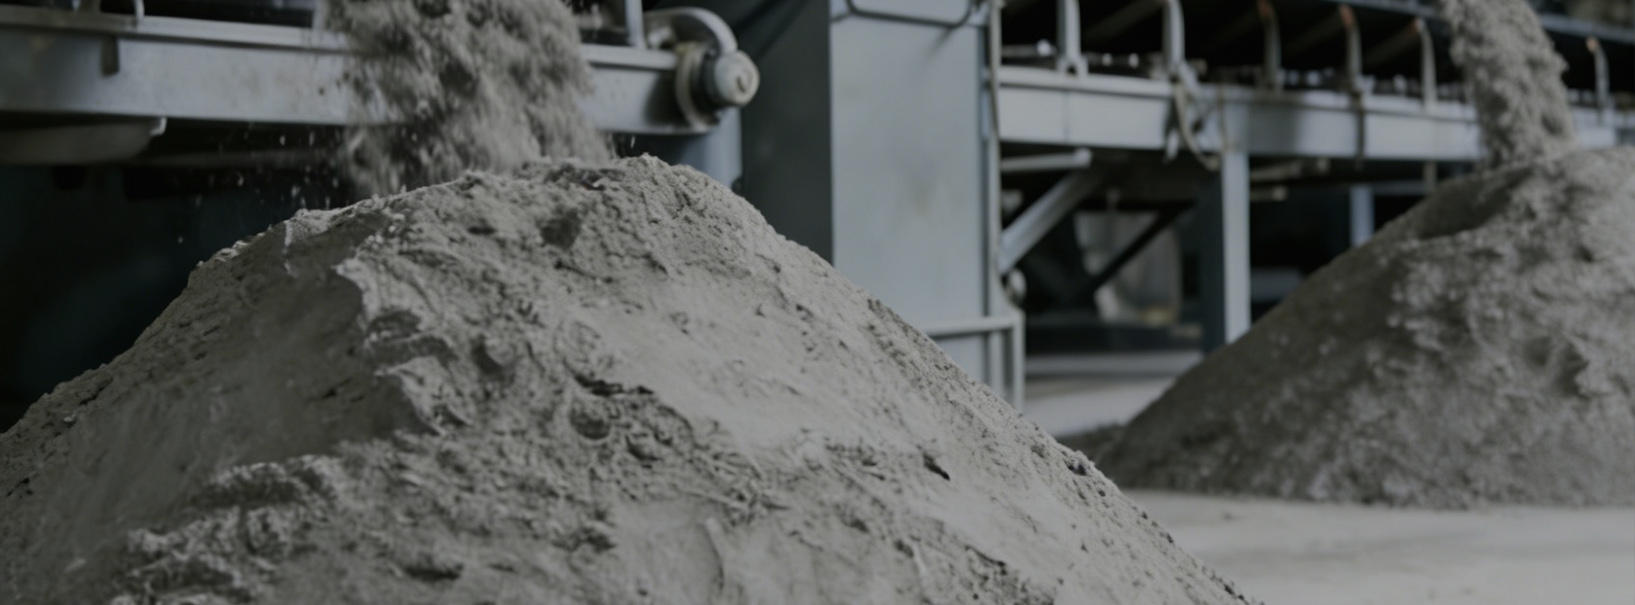
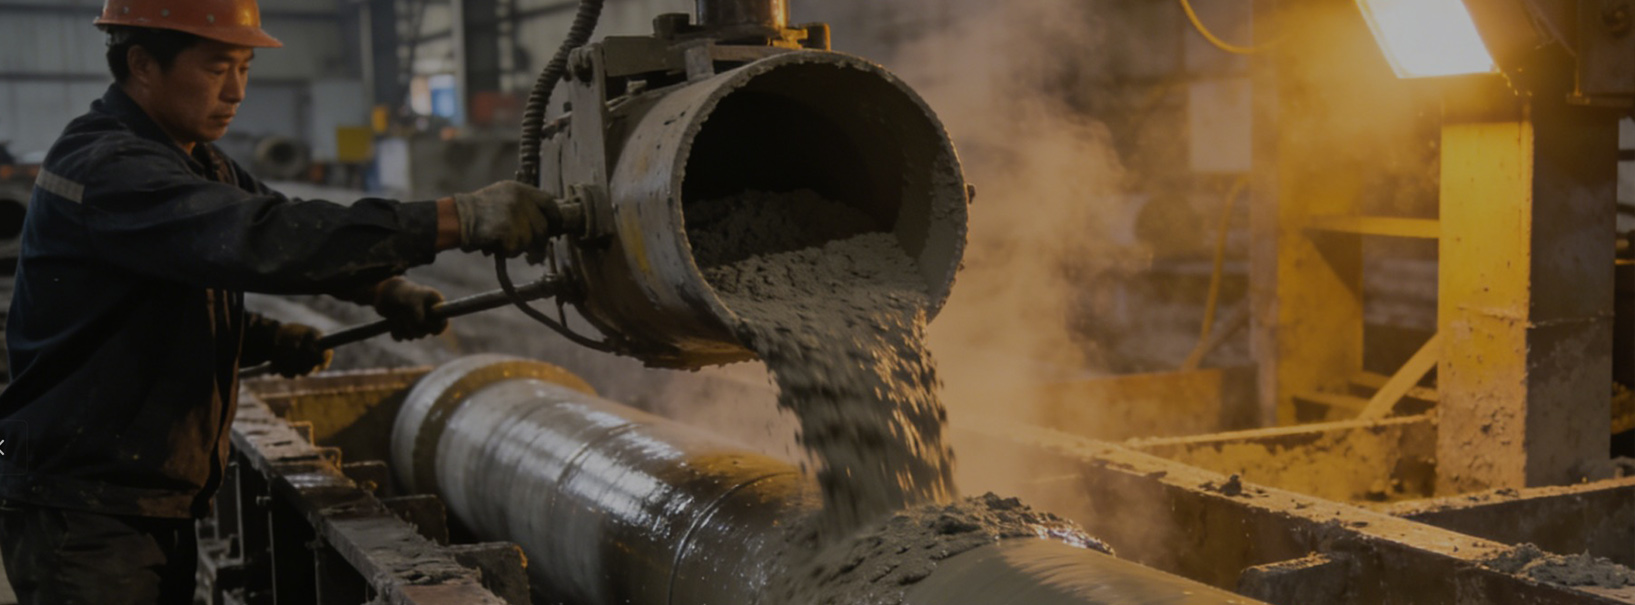
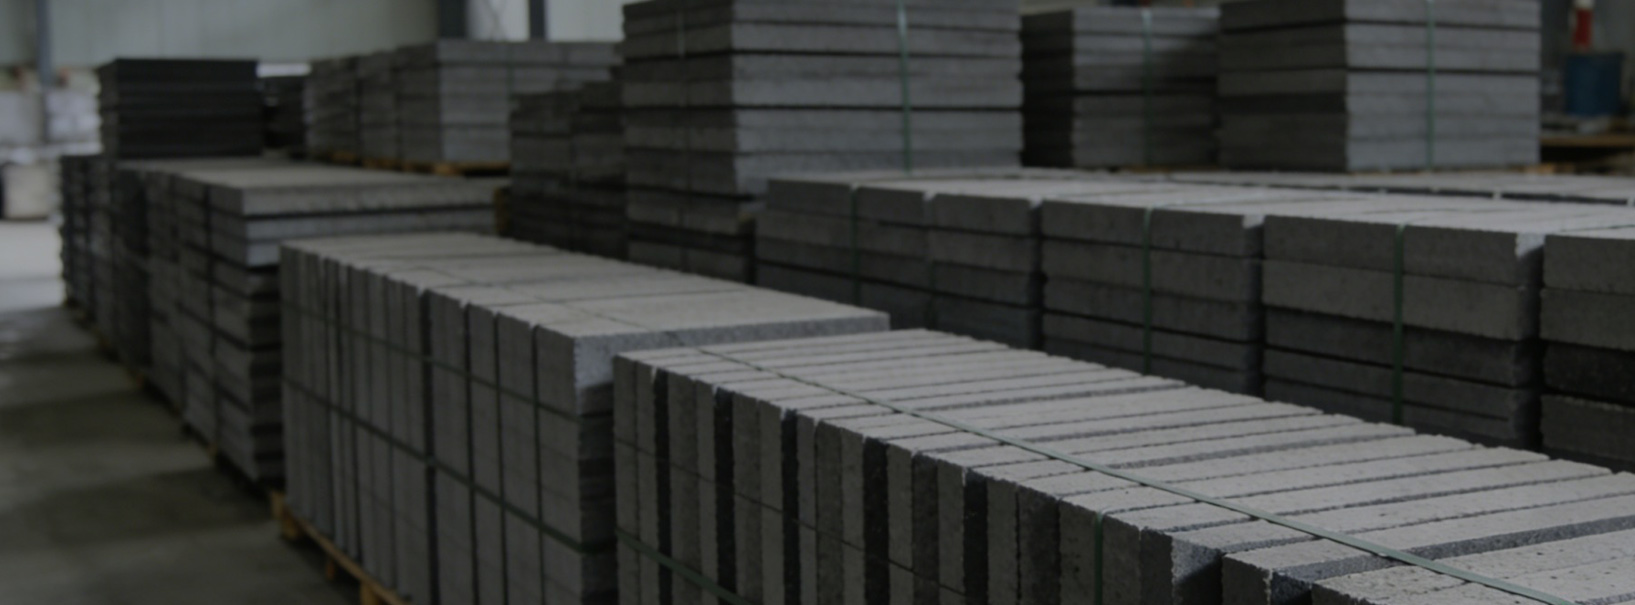
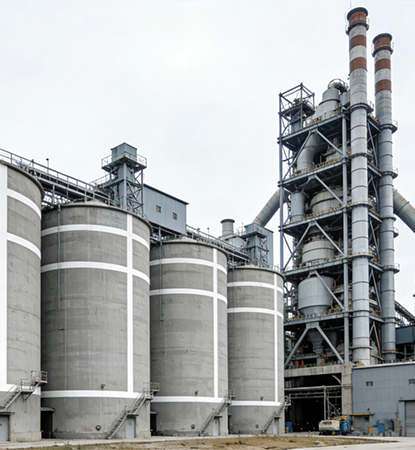
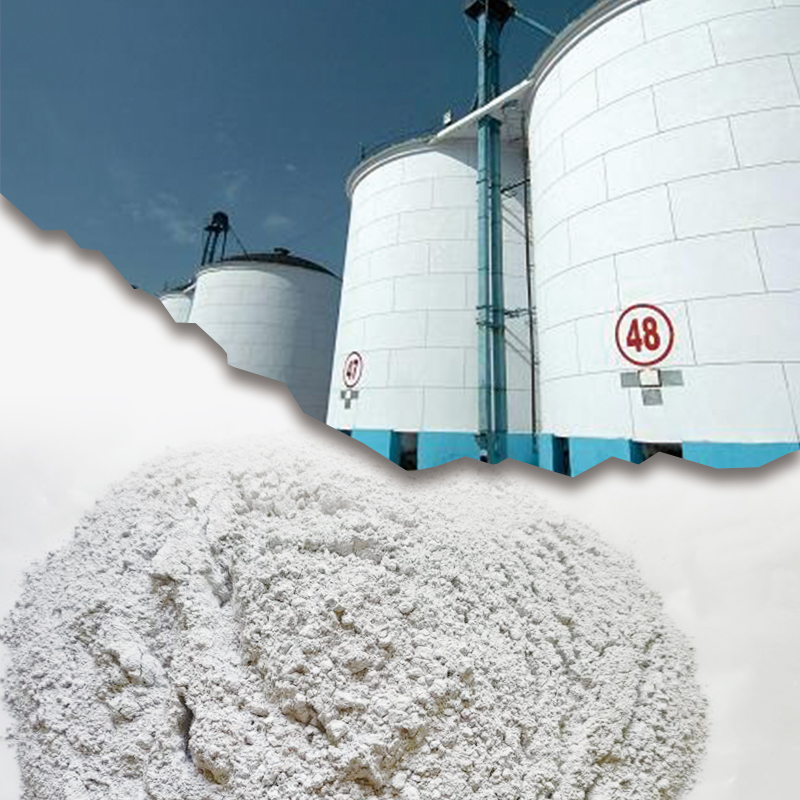
Located within the Guji Cement Co., Ltd. plant area in Jianhu County, the company operates under a unified management but separate accounting model with Guji. The company's production scale is 200,000 tons of ultrafine powder and 600,000 cubic meters of commercial concrete per year, with annual sales revenue exceeding 200 million yuan.
The main equipment includes one φ3.2×13m ball mill, one φ2.6×13m ball mill, and one concrete mixing system and one wet mortar mixing system.
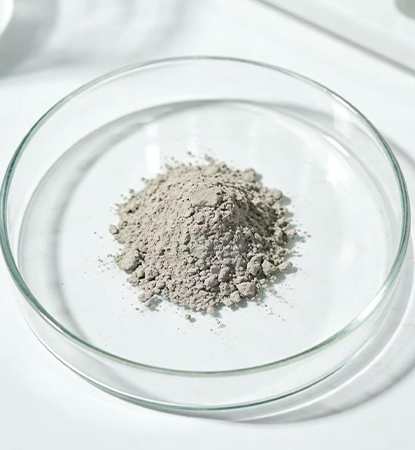
The global ultrafine powder industry has long been synonymous with high-performance construction materials — cement replacement, concrete admixtures, and structural reinforcement. Yet a profound transformation is underway. Today, bulk ultrafine powder for construction is rapidly crossing into advanced medical and pharmaceutical manufacturing, driven by its exceptional particle size control, chemical purity, and engineered surface properties. This convergence is reshaping both industries and creating unprecedented commercial opportunities.
💡 Key Insight: Ultrafine mineral powders with D50 values as low as 14.73μm are now being evaluated for pharmaceutical excipient applications, drug delivery matrices, and sterile facility construction — marking a new era of cross-industry material science.
The global market for ultrafine mineral admixtures — including Ground Granulated Blast Furnace Slag (GGBFS), fly ash blends, and composite ultrafine powders — was valued at over USD 8.2 billion in 2023 and is projected to reach USD 14.6 billion by 2030, growing at a CAGR of approximately 8.4%. China remains the dominant producer, accounting for over 58% of global output, with manufacturers like Jiangsu Anmin New Building Materials Co., Ltd. operating at scales of 200,000 tons per year.
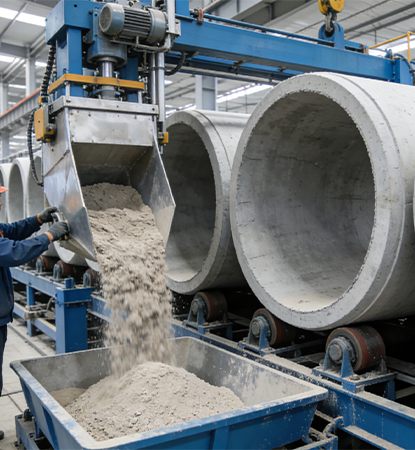
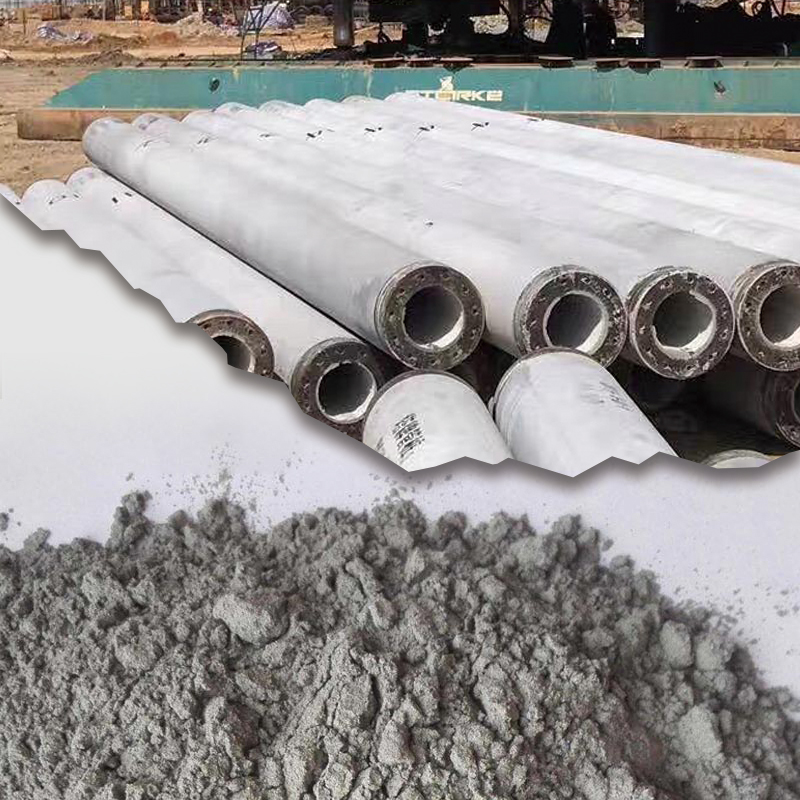
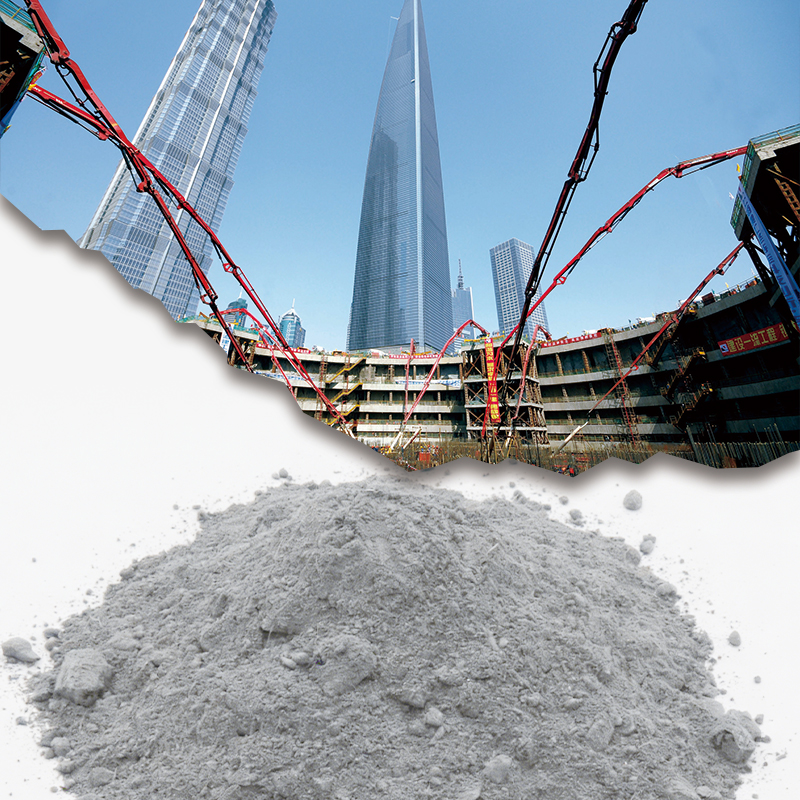
Key commercial drivers include increasingly stringent carbon emission regulations, the global push for green building certifications (LEED, BREEAM), and the cost advantage of ultrafine powder as a partial cement replacement (typically 20–40% substitution rate). In ready-mix concrete, pipe pile manufacturing, and precast elements, ultrafine powder delivers measurable improvements in workability, long-term compressive strength, and durability against chloride ion penetration and sulfate attack.
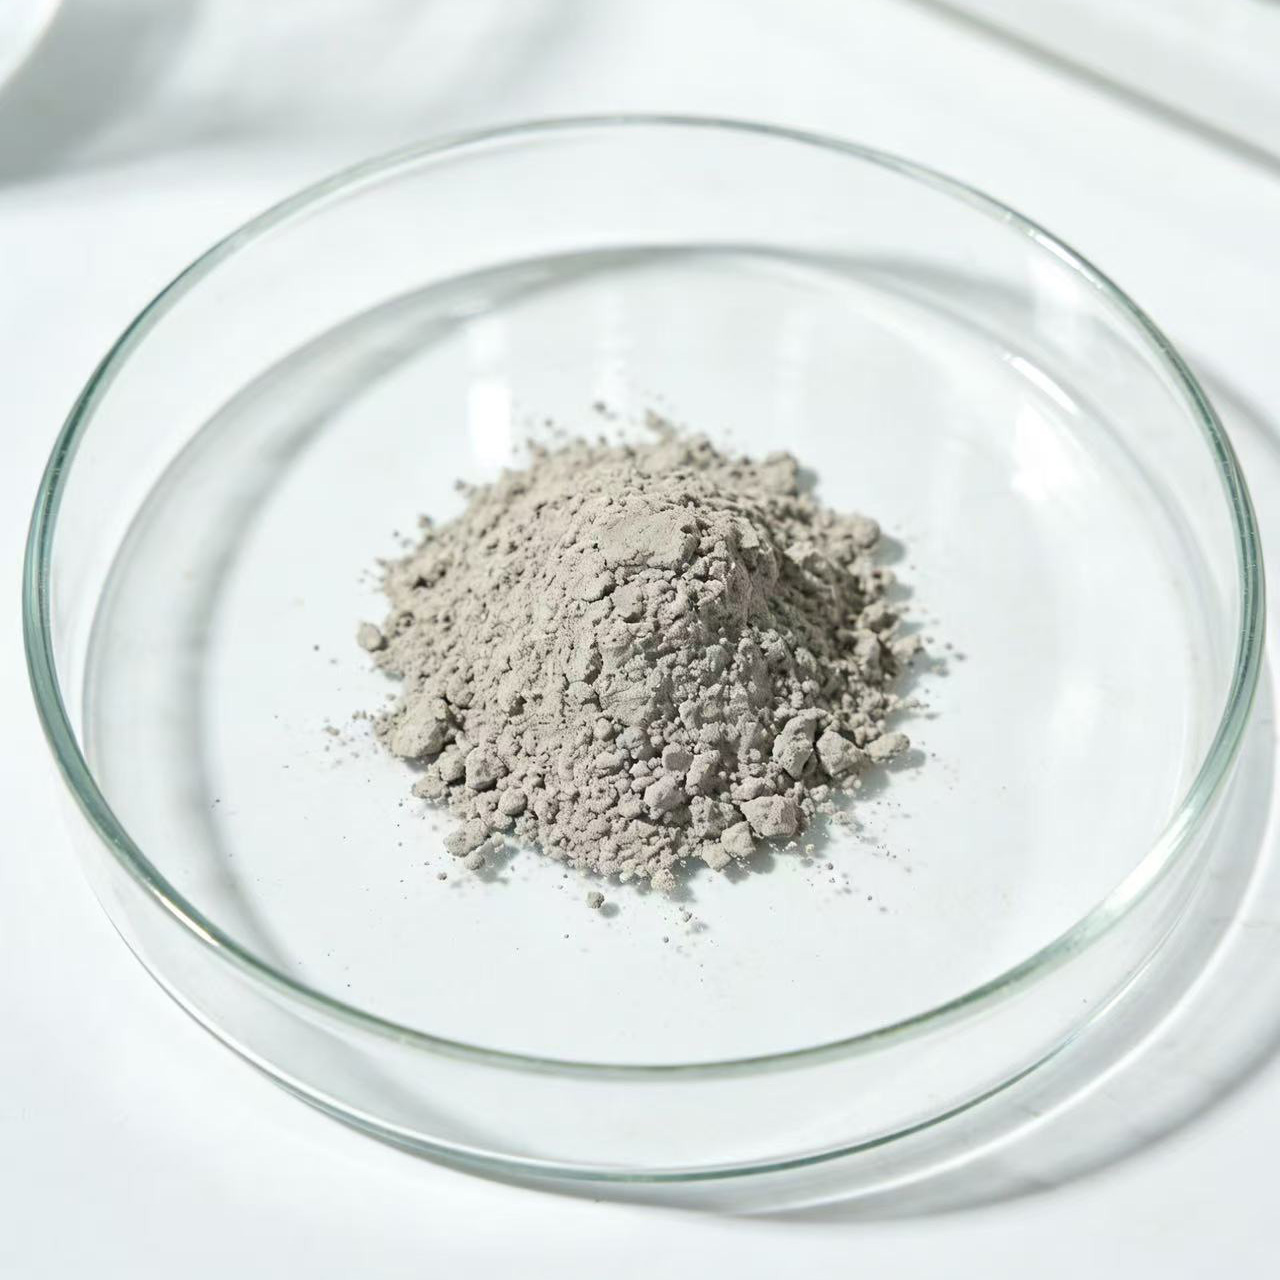
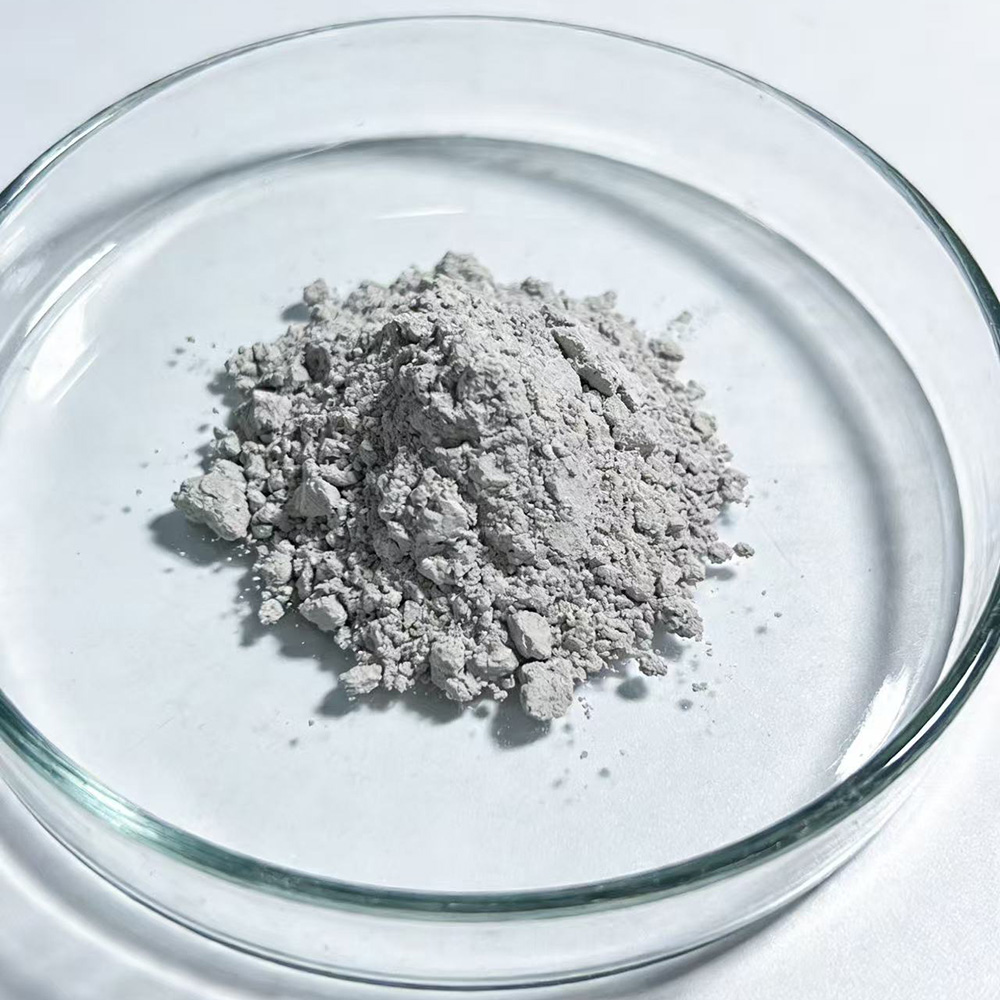
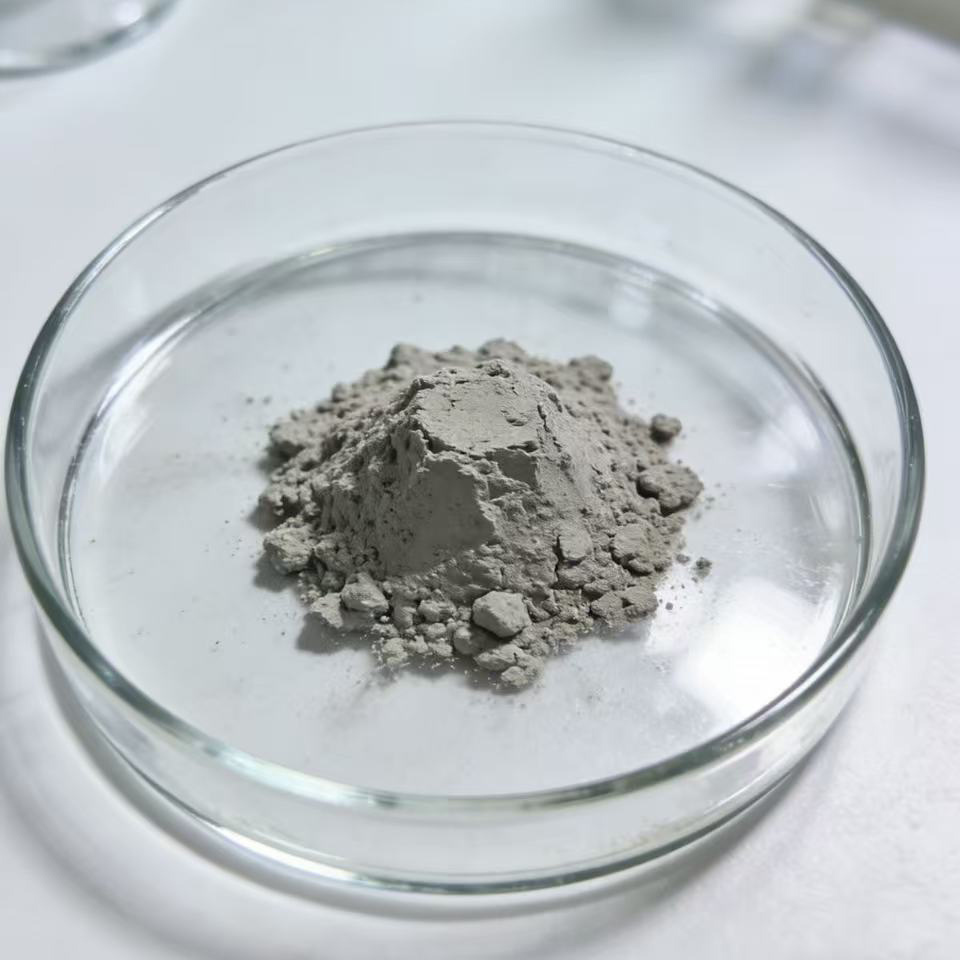
Advanced ball milling achieves D50 = 14.73μm — a specification that bridges construction performance and pharmaceutical excipient standards.
Solid waste valorization (GGBFS, fly ash) reduces CO₂ by up to 40% vs. Portland cement, aligning with global ESG mandates.
200,000 tons/year production capacity ensures reliable bulk supply for both large-scale construction and emerging pharma applications.
The pharmaceutical and medical device sectors are increasingly demanding ultrafine mineral powders for a range of specialized applications. The convergence is not accidental — the same properties that make ultrafine powder ideal for high-performance concrete (particle size distribution, pozzolanic reactivity, low heavy metal content) translate directly into pharmaceutical utility.
Several macro-trends are accelerating the adoption of construction-grade ultrafine powder in medical and pharmaceutical contexts:
Machine learning models now optimize ball mill parameters in real time, achieving target particle size distributions with ±0.5μm precision — enabling pharmaceutical-grade consistency from industrial-scale equipment.
Pharmaceutical companies are partnering with construction material producers to co-develop ultrafine powders from industrial by-products that meet dual-use specifications — reducing material costs by 15–25%.
Global healthcare construction spending is projected to exceed USD 890 billion by 2027, creating massive demand for specialized ultrafine powder in hospital, laboratory, and cleanroom construction.
Ongoing ISO 10993 biocompatibility testing of aluminosilicate ultrafine powders is opening regulatory pathways for medical-grade certification, potentially unlocking a USD 3.2 billion excipient market.
Post-pandemic reshoring of pharmaceutical manufacturing is driving demand for locally produced, high-purity ultrafine powders — creating new opportunities for Chinese manufacturers with GMP-aligned production systems.
Real-time particle size analyzers, XRF elemental analyzers, and blockchain-based batch traceability systems are enabling ultrafine powder manufacturers to meet pharmaceutical documentation standards (CoA, DMF filing).
Scenario 1 — GMP Cleanroom Flooring Systems: Pharmaceutical manufacturing facilities require ISO Class 5–8 cleanrooms with floors that withstand chemical sterilization, electrostatic discharge, and heavy forklift traffic. Ultrafine GGBFS-fly ash blend concrete (D50 ≈ 14.73μm) achieves surface roughness values below Ra 0.8μm after polishing — meeting FDA 21 CFR Part 211 facility standards while offering 30% cost savings over epoxy-only systems.
Scenario 2 — Hospital Radiation Shielding Concrete: Linear accelerator (LINAC) vaults and nuclear medicine hot labs require concrete with densities exceeding 3,500 kg/m³. Ultrafine barite powder (D50 < 20μm) as a cement replacement achieves superior packing density, eliminates macro-voids, and provides attenuation coefficients compliant with NCRP Report No. 151 — critical for protecting patients and staff from ionizing radiation.
Scenario 3 — Pharmaceutical Excipient Grade Calcium Silicate: Construction-derived ultrafine calcium silicate, when subjected to additional purification (acid washing, calcination at 800°C), achieves heavy metal content below 10 ppm — meeting USP <661> and EP 3.1.1 standards for pharmaceutical container and excipient materials. Early-stage commercial partnerships between building material producers and pharma excipient companies are already emerging in Europe and Asia.
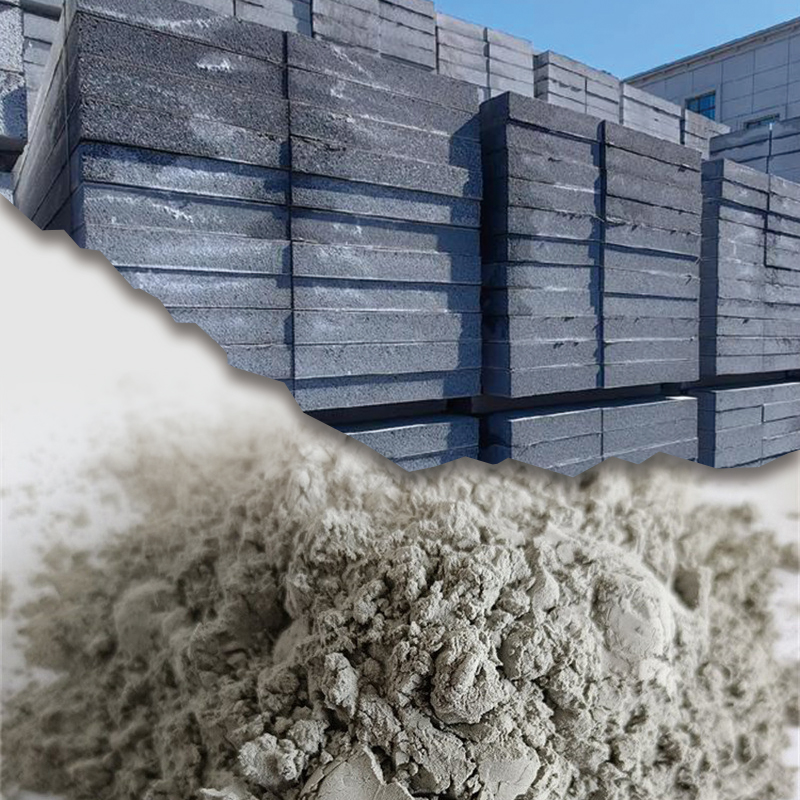
Scenario 4 — Graphite-Modified Insulation Boards for Cold Chain Pharma Storage: A breakthrough application involves ultrafine powder in graphite-modified cement-based insulation boards for pharmaceutical cold chain warehouses. These boards achieve thermal conductivity as low as 0.028 W/(m·K) — comparable to polyurethane foam — while being non-combustible (Class A fire rating), enabling compliant storage of temperature-sensitive biologics and vaccines.
Scenario 5 — Dental Cement & Bone Substitute Materials: Ultrafine aluminosilicate powders processed to pharmaceutical purity are being formulated into glass ionomer dental cements and synthetic bone graft substitutes. Their inherent fluoride release, bioactivity, and compressive strength (up to 220 MPa) make them superior to conventional hydroxyapatite in load-bearing orthopedic applications.
🚀 Strategic Outlook: Manufacturers who invest in dual-certification production lines — meeting both GB/T 18046 (GGBFS standard) and ISO 9001/GMP pharmaceutical quality systems — will capture disproportionate value as the construction-to-pharma material convergence accelerates through 2030.
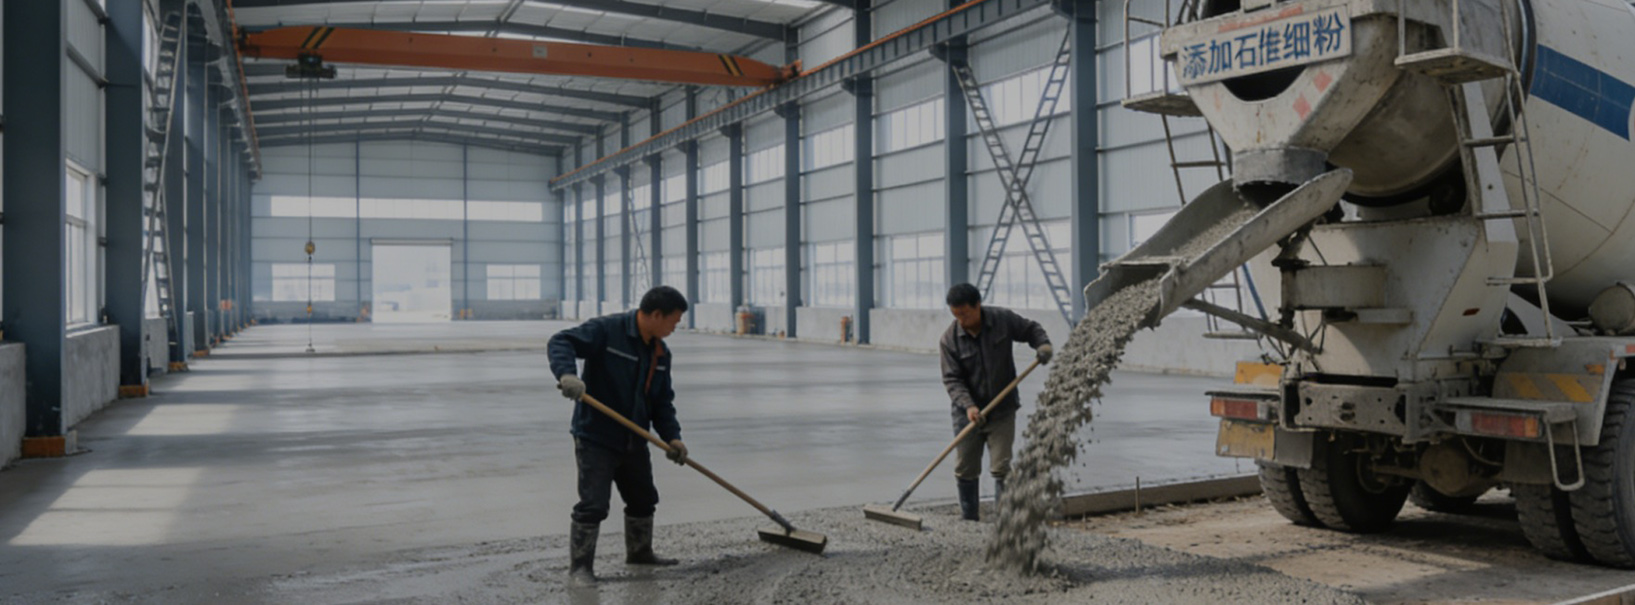
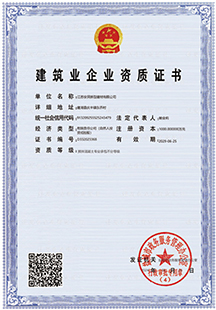
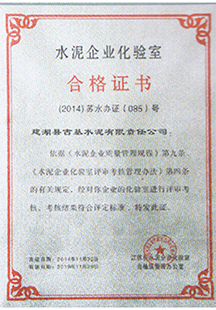
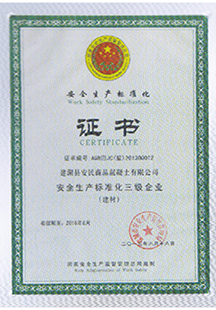
IATF 16949 · CE · FMEA · PPAP · APQP · SPC AND MSA — 100% TEST
 Send
Email
 Phone