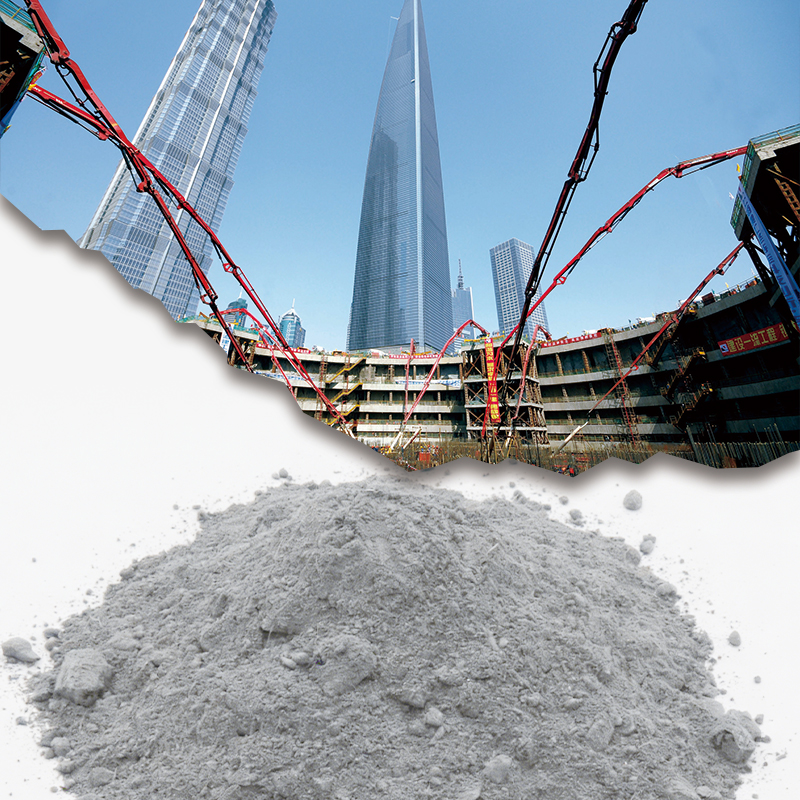
Where there's space - there's possibility

Leave Your Message
Where there's space - there's possibility
Engineered for superior dispersion, ultra-low heavy metal contamination, tailored surface porosity, and unmatched structural integrity across biomedical and ultra-clean pharmaceutical environments.
The global intersection of mineral micro-pulverization and advanced life sciences represents a multi-billion-dollar shift toward high-purity inorganic excipients, bioactive matrices, and aseptic infrastructure.
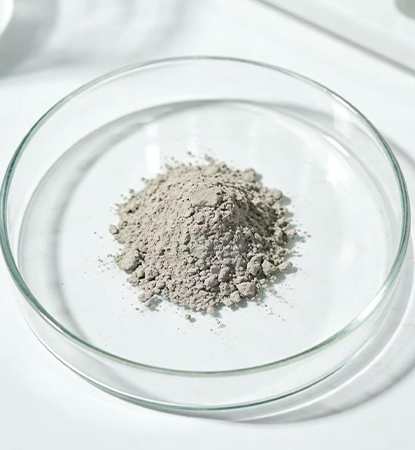
Transitioning from standard bulk carrier powders to tailored ultrafine mineral particles (D50 < 5-15 μm) enables unprecedented API bioavailability, micro-encapsulation stability, and optimized dissolution dynamics in tablet compression and enteric systems.
With stringent pharmacopeial standards (USP, EP, JP), medical-grade inorganic processing demands sophisticated beneficiation, air classification, and magnetic separation to ensure heavy metal levels remain strictly under ultra-trace limits (Pb, As, Cd < 0.1 ppm).
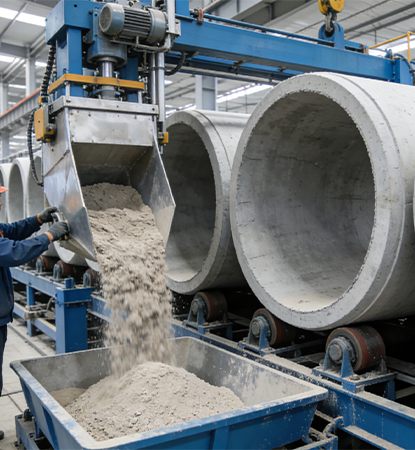
Pharmaceutical production facilities require non-dusting, radiation-shielding, and non-porous antimicrobial flooring and walls. Ultrafine mineral blends create hyper-dense pozzolanic microstructures that resist chemical disinfection and microbial anchoring.
The production of ultrafine mineral powders suitable for high-precision applications relies on high-energy grinding mills integrated with multi-stage dynamic air classifiers. By engineering specific particle shape factors, spherical morphology, and narrow particle size distribution (PSD), manufacturers overcome traditional agglomeration challenges.
Beyond bulk applications, surface-modified inorganic silicate and aluminosilicate micro-powders serve as advanced delivery systems. In dental restorative cements and orthobiological implants, ultrafine calcium-silicate hydrate (C-S-H) phases stimulate hydroxyapatite mineralization while sustaining slow-release therapeutic agents.
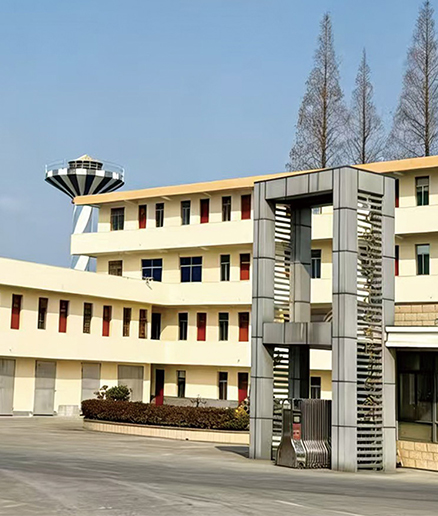
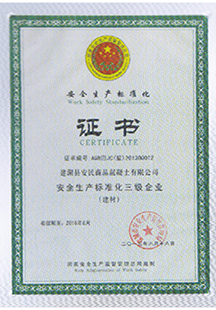
Jiangsu Anmin New Building Materials Co., Ltd., established in 2010, is an important measure in our product extension strategy.
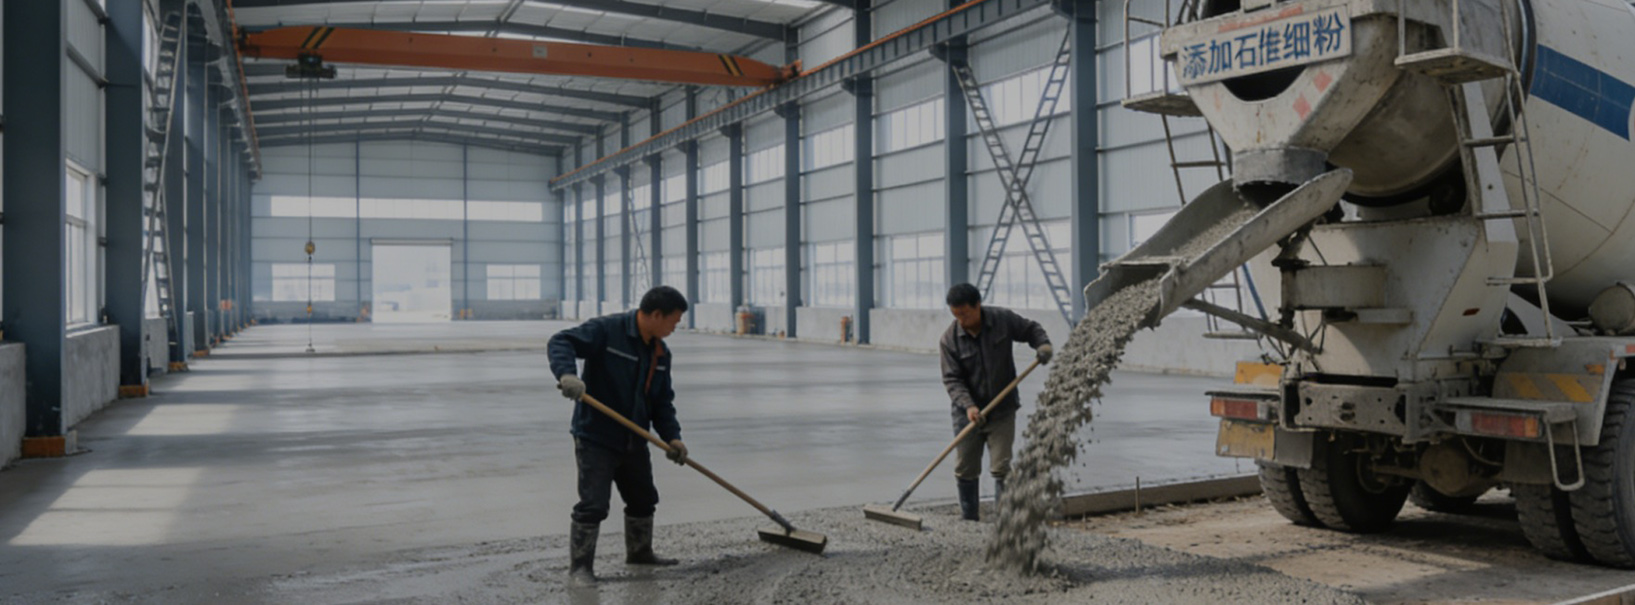
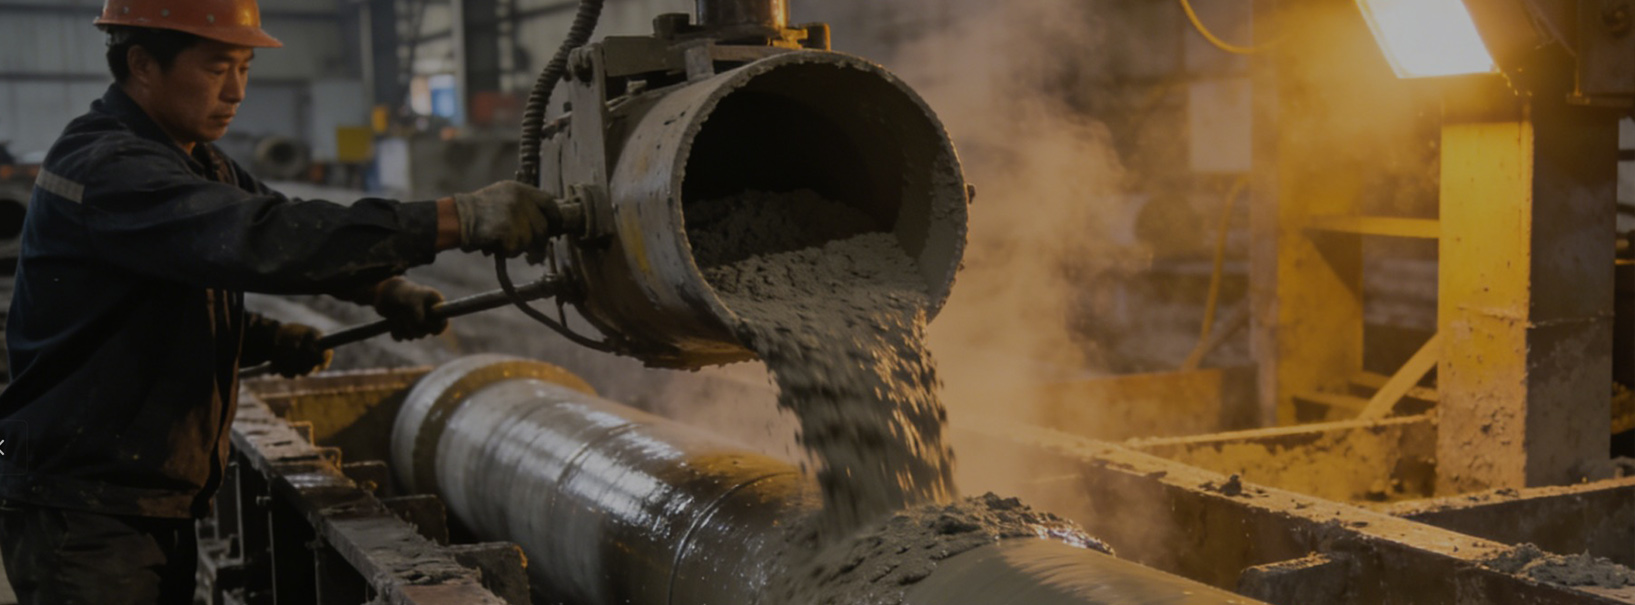
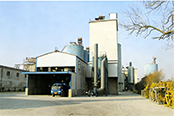
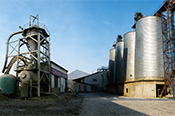
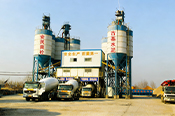
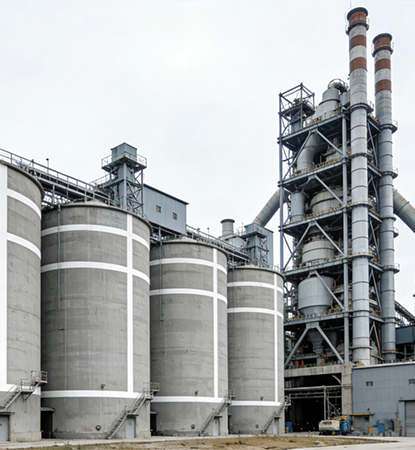
Located within the Guji Cement Co., Ltd. plant area in Jianhu County, the company operates under a unified management but separate accounting model with Guji. The company's production scale is 200,000 tons of ultrafine powder and 600,000 cubic meters of commercial concrete per year, with annual sales revenue exceeding 200 million yuan. The main equipment includes one Φ3.2*13m ball mill, one Φ2.6*13m ball mill, and one concrete mixing system and one wet mortar mixing system.
Showcasing proven field performance across critical structural engineering, specialized concrete curing, emission abatement, and thermal-barrier technological breakthroughs.
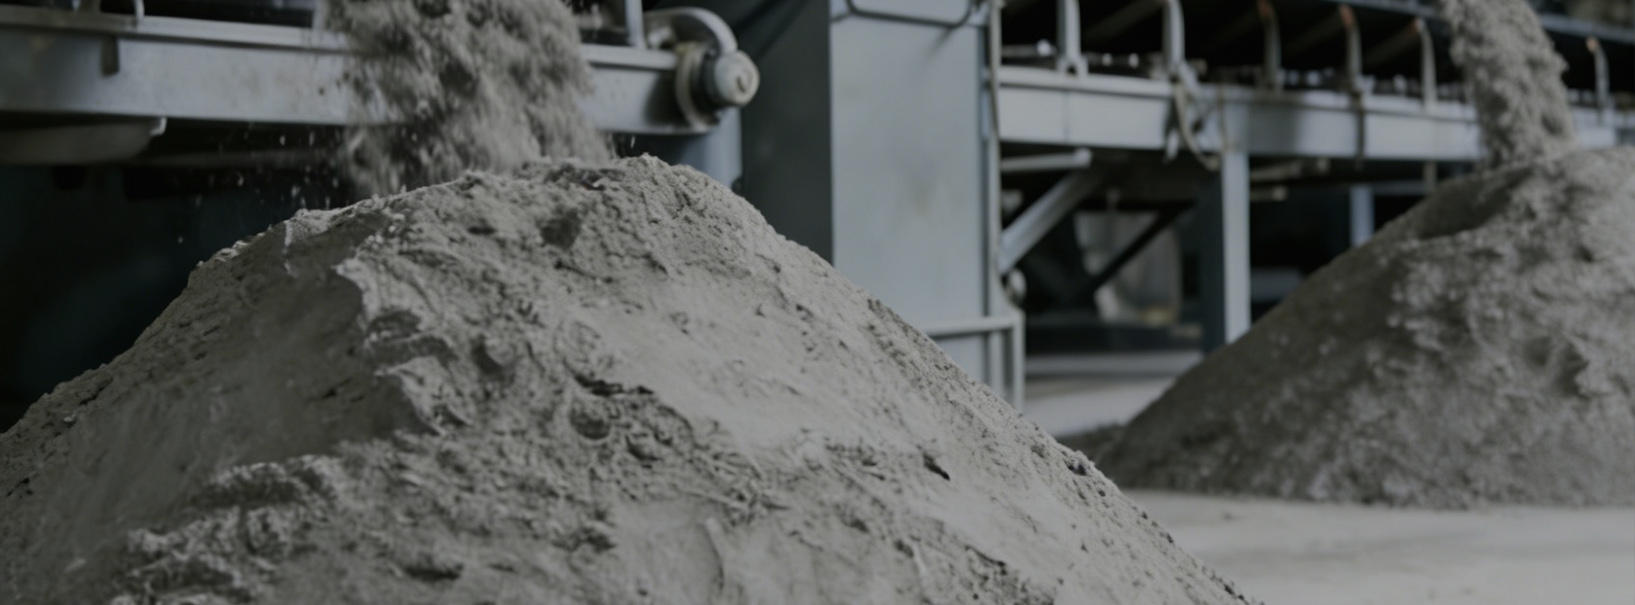
IATF 16949, CE, FMEA, PPAP, APQP, SPC AND MSA 100% TESTED
Precision-milled ultrafine powders, micro-fine composite binders, and high-performance industrial mineral additives engineered to exact chemical and physical tolerances.
Stay updated on the latest breakthroughs in sustainable mineral binders, high-performance manufacturing standards, and cutting-edge industrial material applications.
 Send
Email
 Phone