Where there's space - there's possibility

Leave Your Message
Where there's space - there's possibility
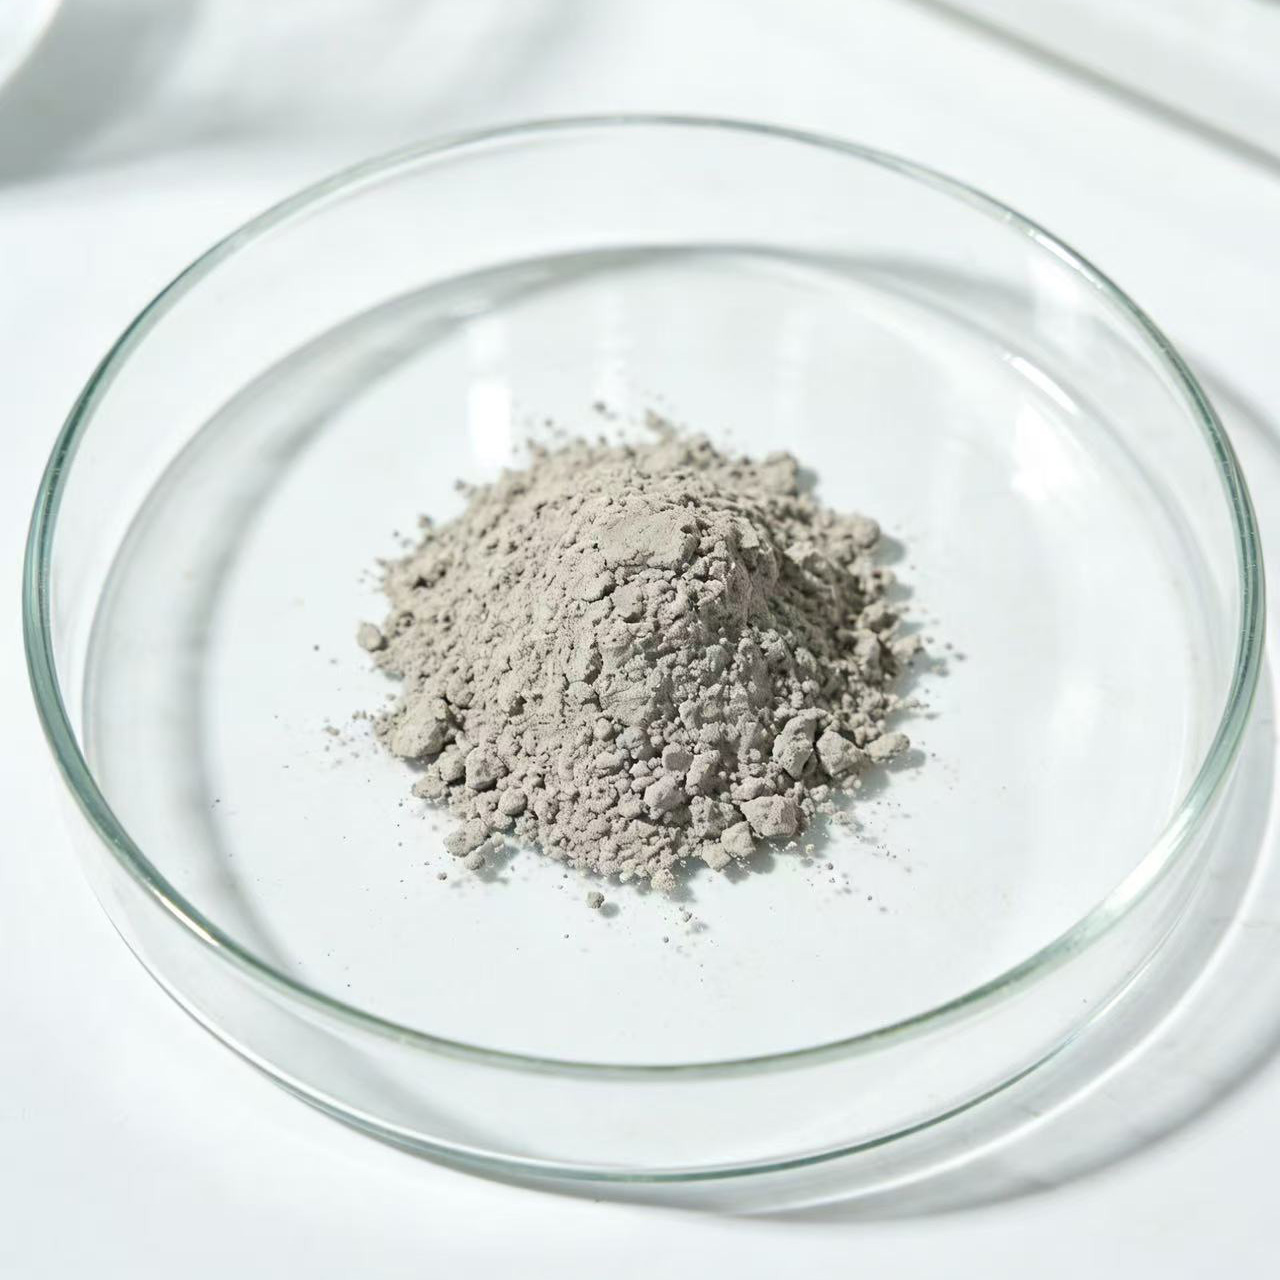
The landscape of modern pharmacology and advanced medical treatments is undergoing a profound transformation, driven largely by innovations in materials science. At the forefront of this revolution is Ultrafine Powder for Advanced Medical and Pharmacy. Historically utilized in industrial applications, the meticulous refinement of particle size distribution—often reaching sub-micron or nanometer scales—has unlocked unprecedented therapeutic potentials. By drastically increasing the surface area-to-volume ratio, ultrafine powders enhance the dissolution rates of poorly water-soluble active pharmaceutical ingredients (APIs), thereby maximizing bioavailability and clinical efficacy.
In the contemporary commercial and industrial landscape, the pharmaceutical ultrafine powder market is experiencing exponential growth. Global pharmaceutical giants are increasingly abandoning traditional milling techniques in favor of advanced micronization technologies, such as cryogenic jet milling and AI-optimized ball milling. This shift is not merely a trend but a regulatory and clinical necessity. With over 40% of newly developed chemical entities classified as poorly soluble (BCS Class II and IV), ultrafine powder processing is the critical bridge between drug discovery and viable commercial formulation. The industrial infrastructure required to produce these medical-grade powders must adhere strictly to Good Manufacturing Practices (GMP), ensuring zero contamination, precise particle size control, and absolute batch-to-batch consistency.
Economically, the integration of ultrafine excipients and APIs reduces the required dosage, minimizing potential side effects for patients while significantly lowering active material costs for manufacturers. This dual benefit—enhancing patient compliance and optimizing production economics—cements ultrafine powder technology as a cornerstone of next-generation pharmaceutical manufacturing.
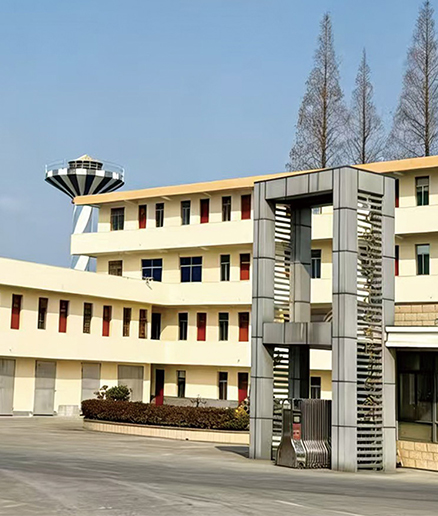
Jiangsu Anmin New Building Materials Co., Ltd., established in 2010, is an important measure in our product extension strategy. While our roots lie in robust material processing, our advanced milling infrastructure forms the foundation for scalable, high-precision powder manufacturing applicable across diverse high-tech industries.
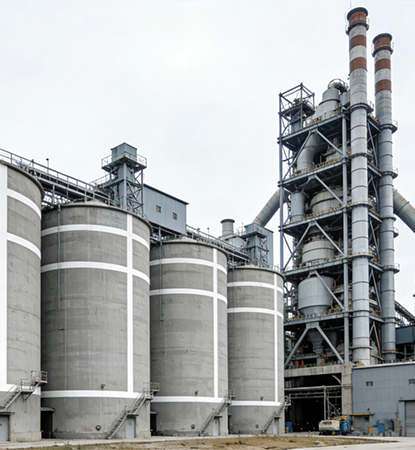
Located within the Guji Cement Co., Ltd. plant area in Jianhu County, the company operates under a unified management but separate accounting model with Guji. The company's production scale is 200,000 tons of ultrafine powder and 600,000 cubic meters of commercial concrete per year, with annual sales revenue exceeding 200 million yuan. The main equipment includes one φ3.2*13m ball mill, one φ2.6*13m ball mill, and advanced mixing systems. This massive processing capability demonstrates our expertise in particle size reduction, a principle directly translatable to the rigorous demands of advanced excipient manufacturing.
The versatility of Ultrafine Powder extends far beyond simple oral solid dosages. By manipulating physical properties at the micro and nano levels, researchers are unlocking targeted therapies and advanced medical devices that were previously relegated to science fiction. Let us explore the most critical application scenarios driving current medical innovation.
In oncology and systemic disease treatment, protecting the API until it reaches the specific site of action is paramount. Ultrafine powders serve as the core matrix for nanocarriers and liposomes. Their uniform particle size ensures predictable degradation rates and controlled release profiles, minimizing systemic toxicity while maximizing therapeutic impact at the cellular level.
Dry Powder Inhalers (DPIs) require particles to be strictly within the 1 to 5 micrometer aerodynamic diameter range to successfully navigate the respiratory tract and deposit in the deep alveolar regions. Advanced micronization technologies produce ultrafine API and carrier powders (like lactose) with optimal flowability and dispersibility, revolutionizing asthma and COPD treatments.
In orthopedics and dentistry, ultrafine bioactive glass and hydroxyapatite powders are synthesized to mimic natural bone mineral composition. These powders are used to coat titanium implants or formulate injectable bone cements. The ultrafine nature of the powder accelerates cellular adhesion, osteointegration, and rapid tissue regeneration.
Trauma care relies heavily on rapid hemostasis. Ultrafine powders derived from chitosan, zeolites, or specialized synthetic polymers possess an immense surface area that rapidly absorbs water from blood, concentrating platelets and clotting factors instantly. Their fine particle size allows them to conform perfectly to irregular wound geometries, providing life-saving interventions in surgical and emergency settings.
The future of pharmacy lies in personalized dosages. Ultrafine powders are the essential "ink" for 3D printing pharmaceutical tablets. The rheological properties of these powders ensure smooth extrusion and precise layer-by-layer deposition, allowing pharmacists to print multi-drug polypills with customized release kinetics tailored to an individual patient's metabolic profile.
As the pharmaceutical industry transitions towards Industry 4.0, the production of ultrafine powders is becoming increasingly sophisticated. The most prominent development trend is the integration of Artificial Intelligence (AI) and Machine Learning (ML) into the milling and micronization processes. Historically, achieving the perfect particle size distribution (PSD) required extensive trial-and-error, consuming valuable API and time. Today, AI-driven process analytical technologies (PAT) monitor milling dynamics in real-time, utilizing predictive algorithms to adjust mill speed, feed rates, and gas pressures autonomously. This ensures a remarkably narrow PSD, eliminating out-of-spec batches and guaranteeing the highest level of pharmaceutical quality control.
Furthermore, the trend of Green Manufacturing is reshaping how ultrafine powders are produced. Traditional milling often generates excessive heat and consumes vast amounts of energy, which can degrade thermo-sensitive biological drugs. The latest advancements involve cryogenic milling utilizing liquid nitrogen, coupled with energy-recovery systems. This not only preserves the polymorphic stability of complex APIs but also drastically reduces the carbon footprint of pharmaceutical manufacturing facilities.
Looking ahead, the synergy between nanotechnology and ultrafine powders will birth "smart excipients." These are advanced powder matrices designed to respond to specific physiological triggers—such as pH changes in the gastrointestinal tract or specific enzymatic activities—to release the drug exactly when and where it is needed. As companies scale their production capabilities, mastering the physics of ultrafine powders will remain the critical differentiator in developing next-generation therapeutics that are safer, more effective, and accessible globally.
IATF 16949, CE, FMEA, PPAP, APQP, SPC AND MSA 100% TEST
 Send
Email
 Phone
