Where there's space - there's possibility

Leave Your Message
Where there's space - there's possibility
Direct factory supply of high-purity, tightly graded ultrafine mineral powders tailored for advanced industrial composites, specialized electronic insulation, and high-performance structural matrices.
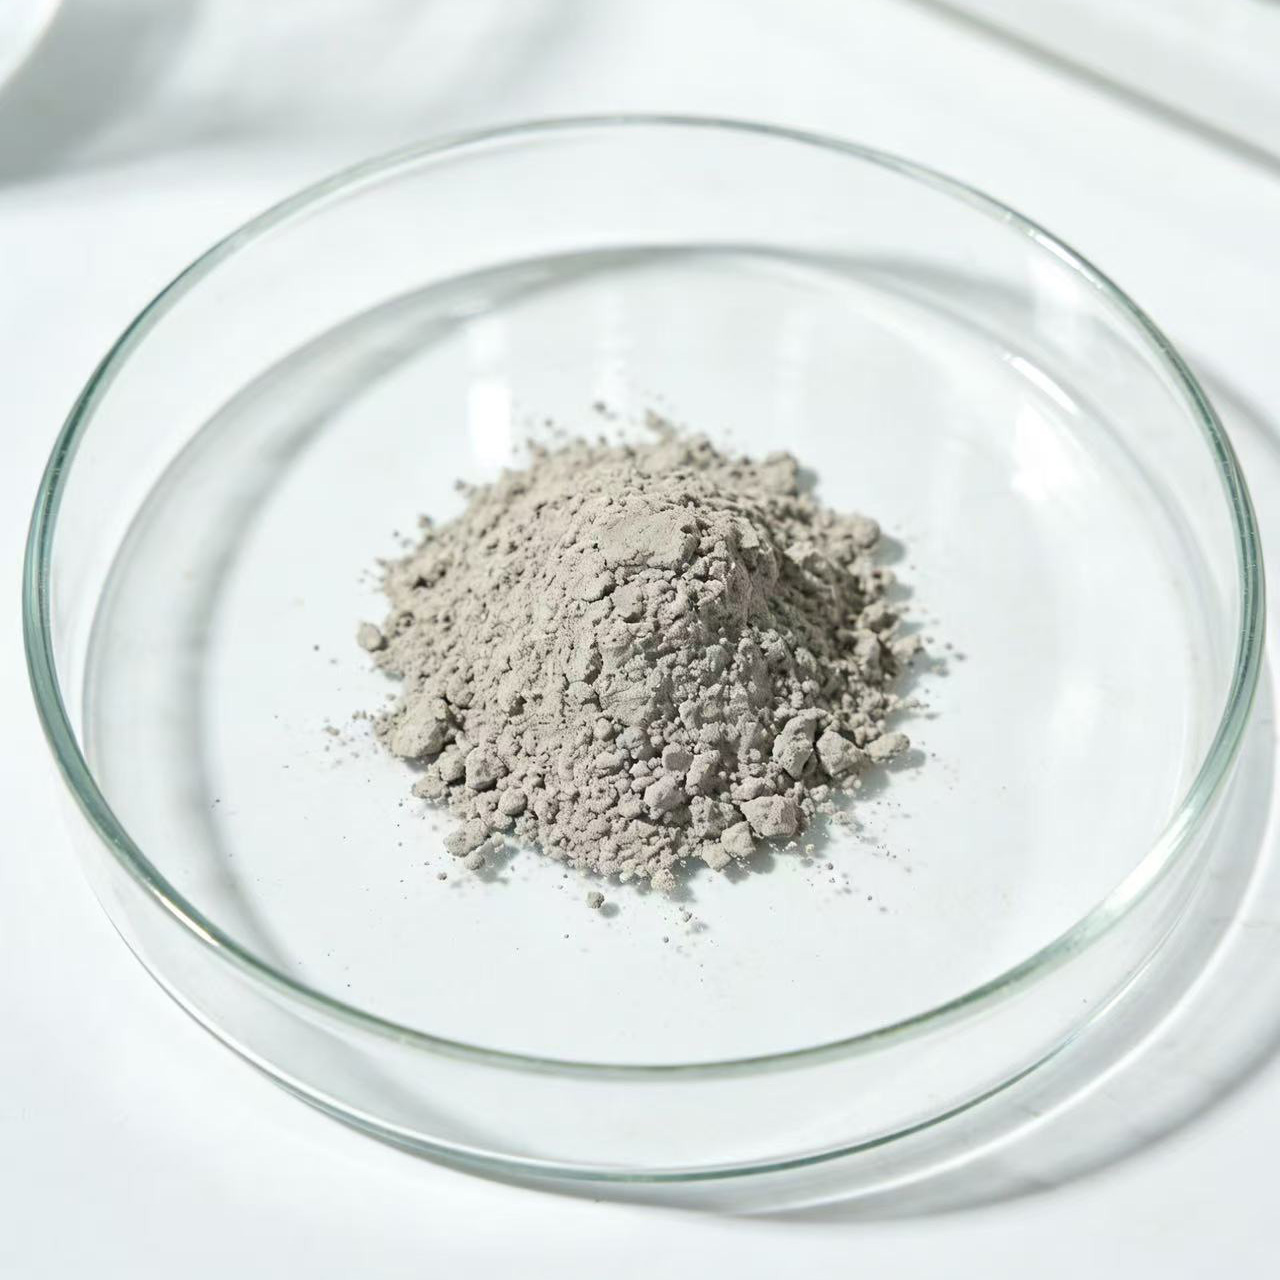
Sub-micron engineered mineral filler with ultra-narrow particle size distribution for high-density electronic substrates and composite matrices.
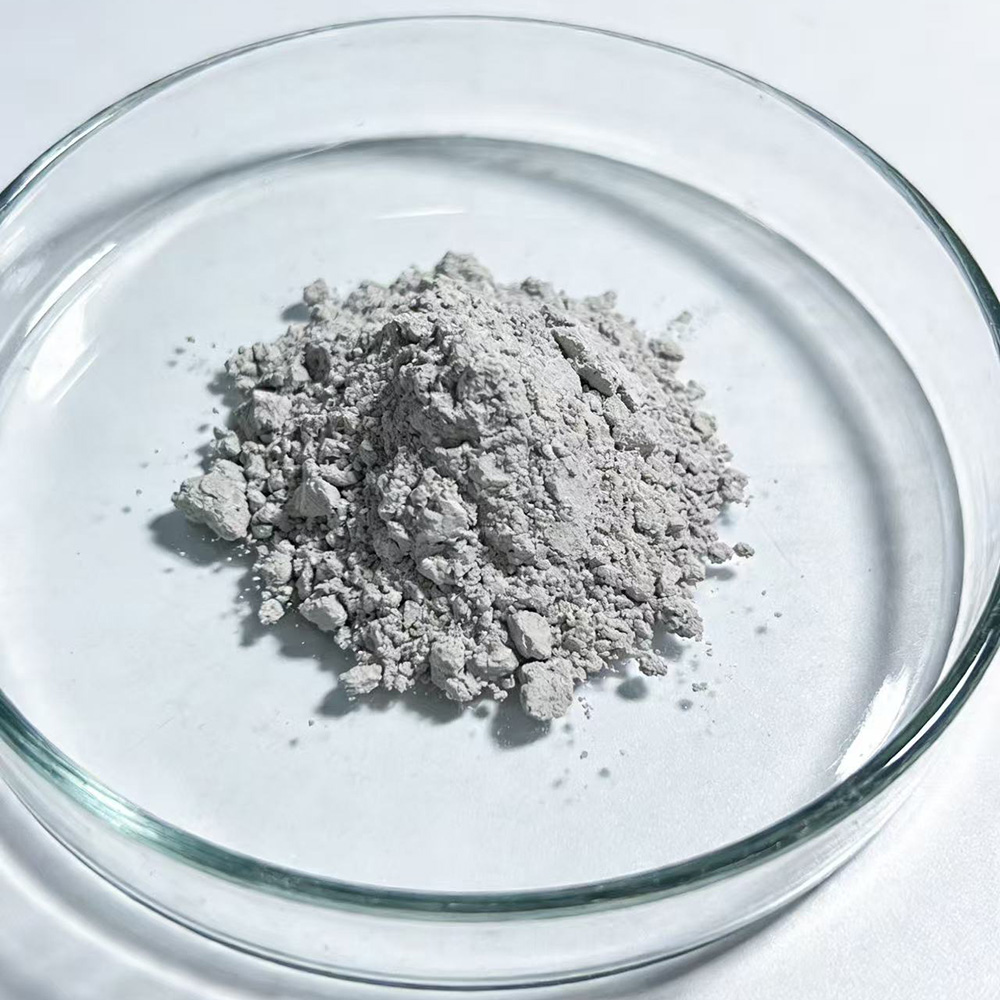
Optimized mineral binder engineered for high workability, stable rheology, and crack-resistant tech containment infrastructures.
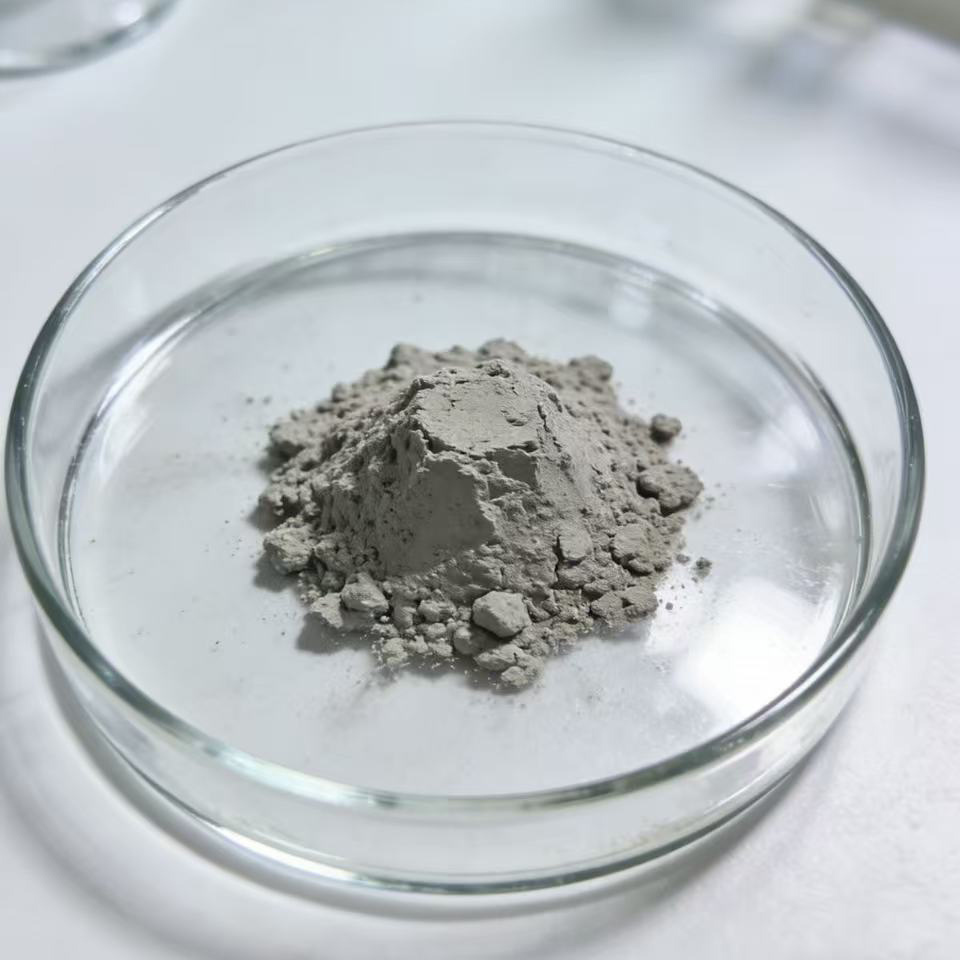
High-grade mineral composite binder delivering superior early and late hydration strengths for high-load cleanrooms and tech plants.
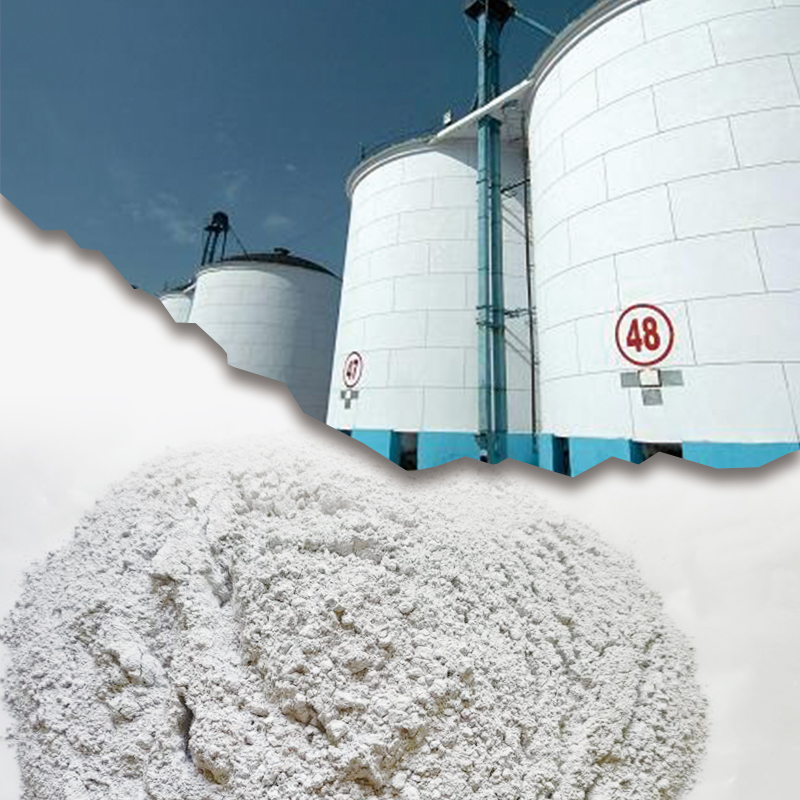
Synergistic GGBFS and fly ash micro-composite providing pozzolanic micro-packing, chemical impermeability, and low thermal expansion.
As artificial intelligence hardware, 5G/6G high-frequency telecommunications, electric vehicles, and precision microelectronics accelerate, the demand for inorganic ultrafine mineral powders has surpassed conventional construction boundaries.
In modern electronic manufacturing, thermal dissipation, dielectric stability, and dimensional tolerance have become critical operational bottlenecks. Ultrafine mineral powders—such as micronized silica, ground granulated blast-furnace slag (GGBFS), fly ash micro-spheres, and functional silicate matrices—serve as indispensable functional micro-fillers. By achieving precise particle size distribution (D50 down to sub-micron scales), these powders maximize packing density, reduce the Coefficient of Thermal Expansion (CTE), and dramatically enhance thermal conductivity in epoxy molding compounds (EMC), thermal interface materials (TIMs), and copper-clad laminates (CCL).
Furthermore, the green transformation in global electronics packaging emphasizes circular supply chains. Upcycling high-purity industrial mineral by-products into high-value ultrafine functional fillers enables hardware manufacturers to achieve aggressive ESG (Environmental, Social, and Governance) targets without compromising physical or electrical reliability.
Ultra-low ionic impurity content ensures exceptional volume resistivity and stable dielectric constants (εr) across wide operating frequency spectrums (1 GHz to 77 GHz).
Spherical and sub-angular morphologies provide superior shear-thinning behavior, enabling filler loading rates up to 70%-88% by weight in polymer matrices without sacrificing mold flow.
Minimizes internal thermal stress during rapid temperature cycling (-55°C to 150°C), eliminating micro-cracking and warpage in semiconductor packages.
Direct wholesale sourcing from large-scale ball milling operations allows tier-1 tech suppliers and industrial formulators to secure high-purity mineral powders at highly competitive pricing, significantly reducing overall manufacturing costs.
Strict laser granulometry controls guarantee accurate particle distribution (D50=14.73μm, D90<30μm, or sub-10μm custom grades), eliminating oversize aggregates and guaranteeing smooth resin impregnation and homogeneous blending.
Manufactured under unified QA workflows complying with IATF 16949, CE, and comprehensive PPAP/APQP methodologies, guaranteeing batch-to-batch chemical stability, low moisture absorption, and predictable curing kinetics.
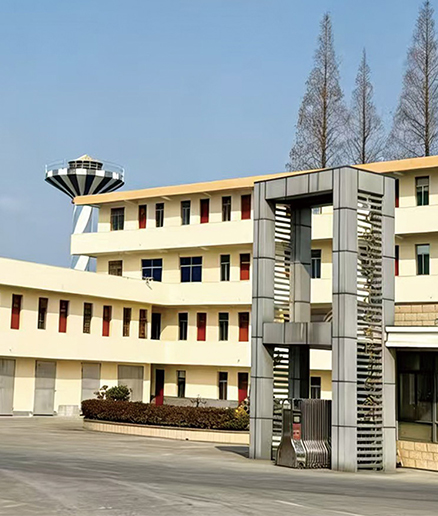
Located within the Guji Cement Co., Ltd. plant area in Jianhu County, the company operates under a unified management but separate accounting model with Guji. The company's production scale is 200,000 tons of ultrafine powder and 600,000 cubic meters of commercial concrete per year, with annual sales revenue exceeding 200 million yuan.
The main manufacturing facilities include state-of-the-art grinding and sorting lines: one φ3.2*13m ball mill, one φ2.6*13m ball mill, an integrated high-precision concrete mixing system, and a dedicated wet mortar mixing system. This industrial muscle guarantees consistent ultrafine processing capability, uniform particle sphericity, and reliable mass supply for high-demand technology, infrastructure, and electronic composite partners worldwide.
Explore how our engineered ultrafine mineral powders optimize micro-structure density, thermal barrier coatings, high-durability enclosures, and low-carbon cementitious tech matrixes across diverse industrial sectors.
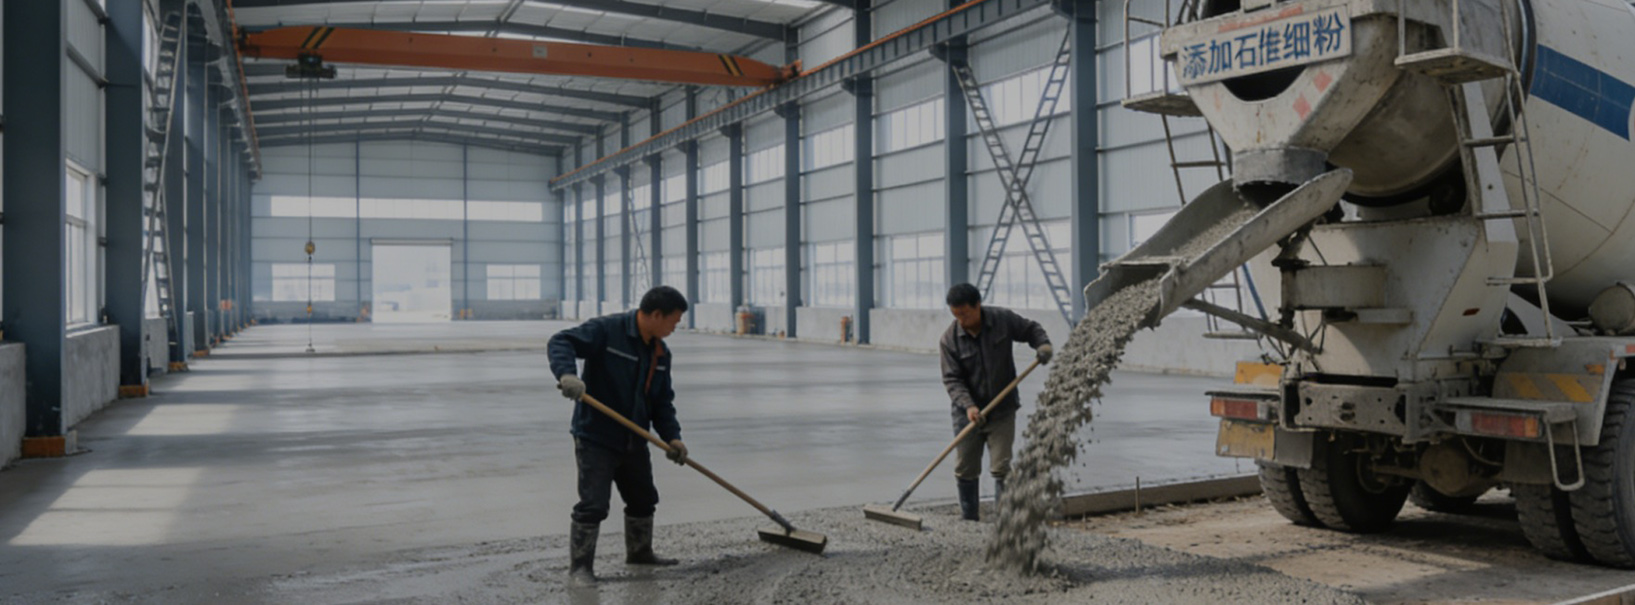
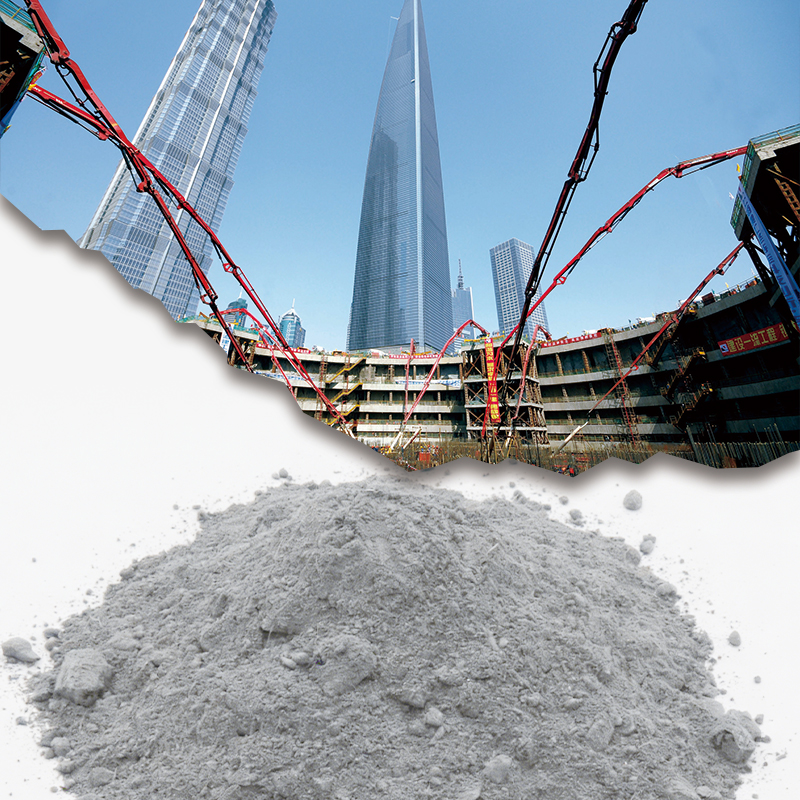
Application in commercial C30 matrixes providing dense micro-pore packing, high early compressive gain, and crack-free surfaces required for electronic cleanrooms and vibration-sensitive fabrication facilities.
View Case Study →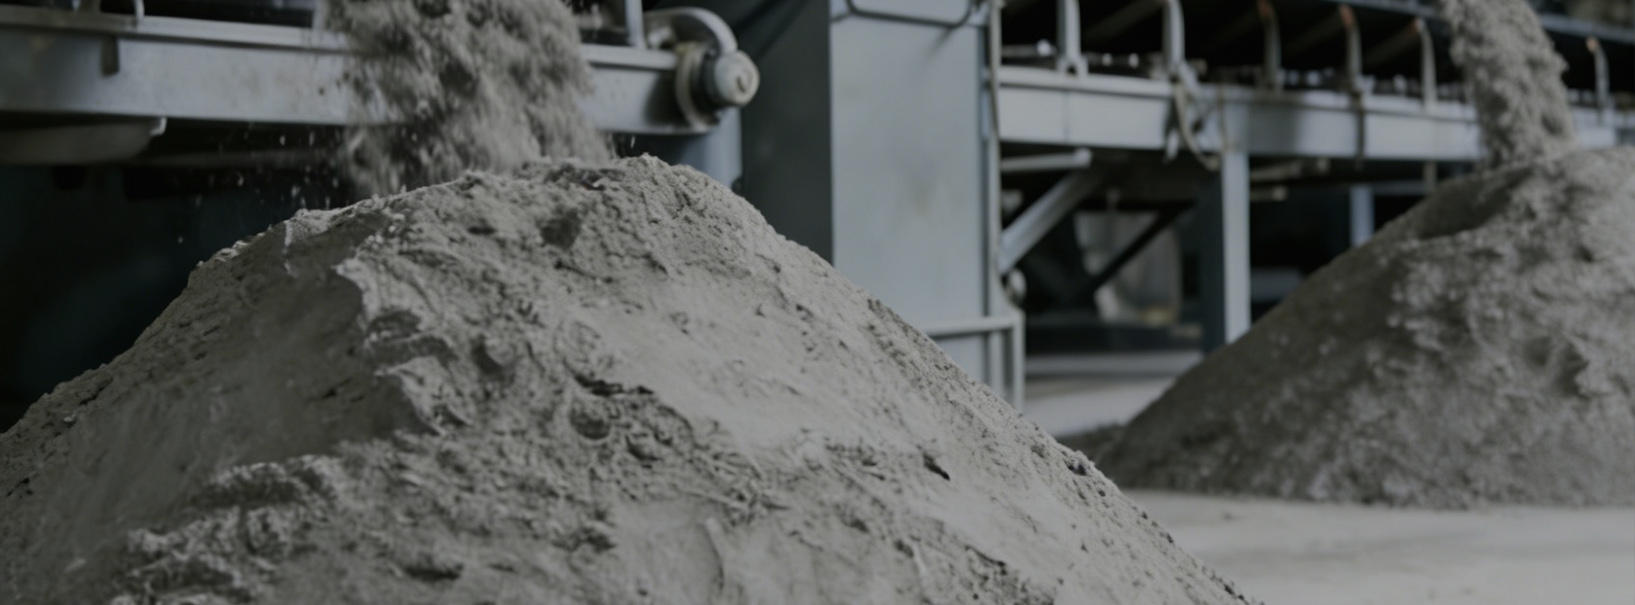
Industrial mineral matrix optimization delivering up to 30% clinker substitution, lowering carbon footprints while accelerating secondary hydration to achieve superior 28-day flexural and compressive ratings.
View Case Study →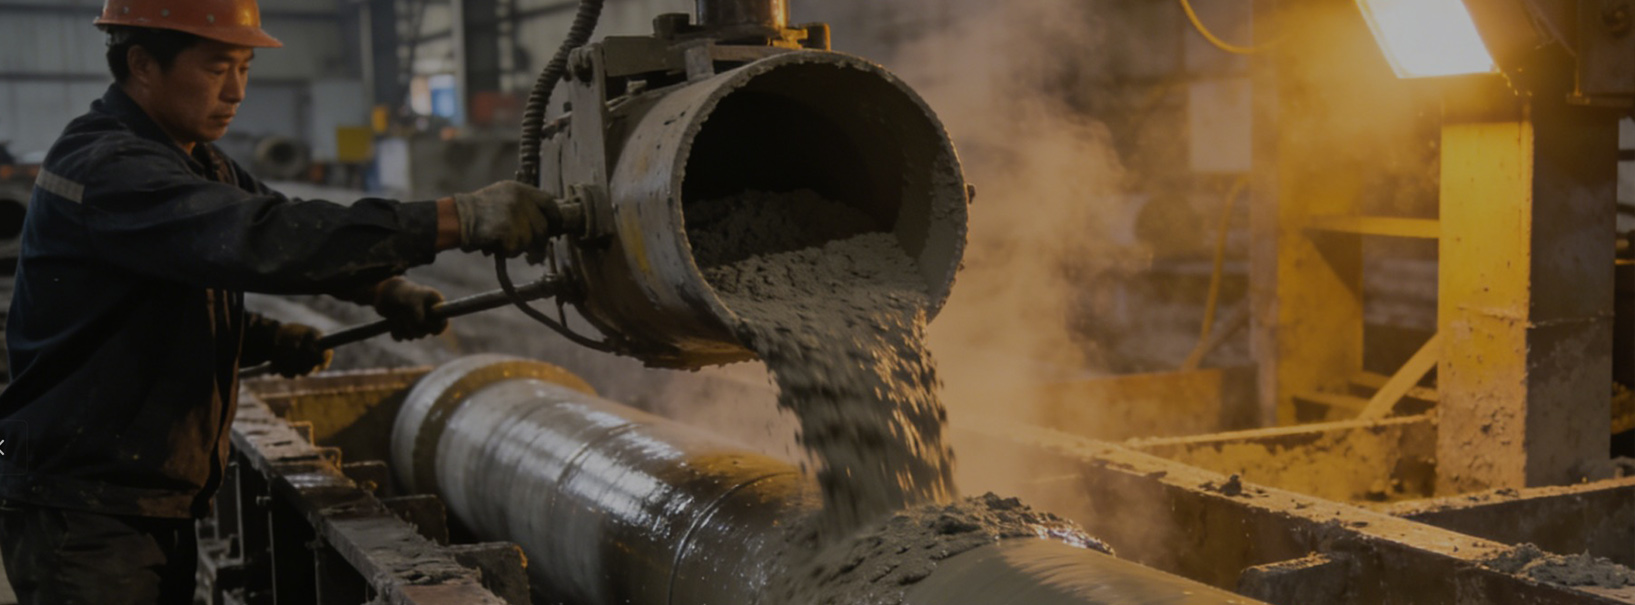
Integration into centrifugal precast pipe piles and cable ducts, increasing dynamic slurry fluidity, reducing water-binder ratio, and eliminating demolding micro-defects under accelerated steam cycles.
View Case Study →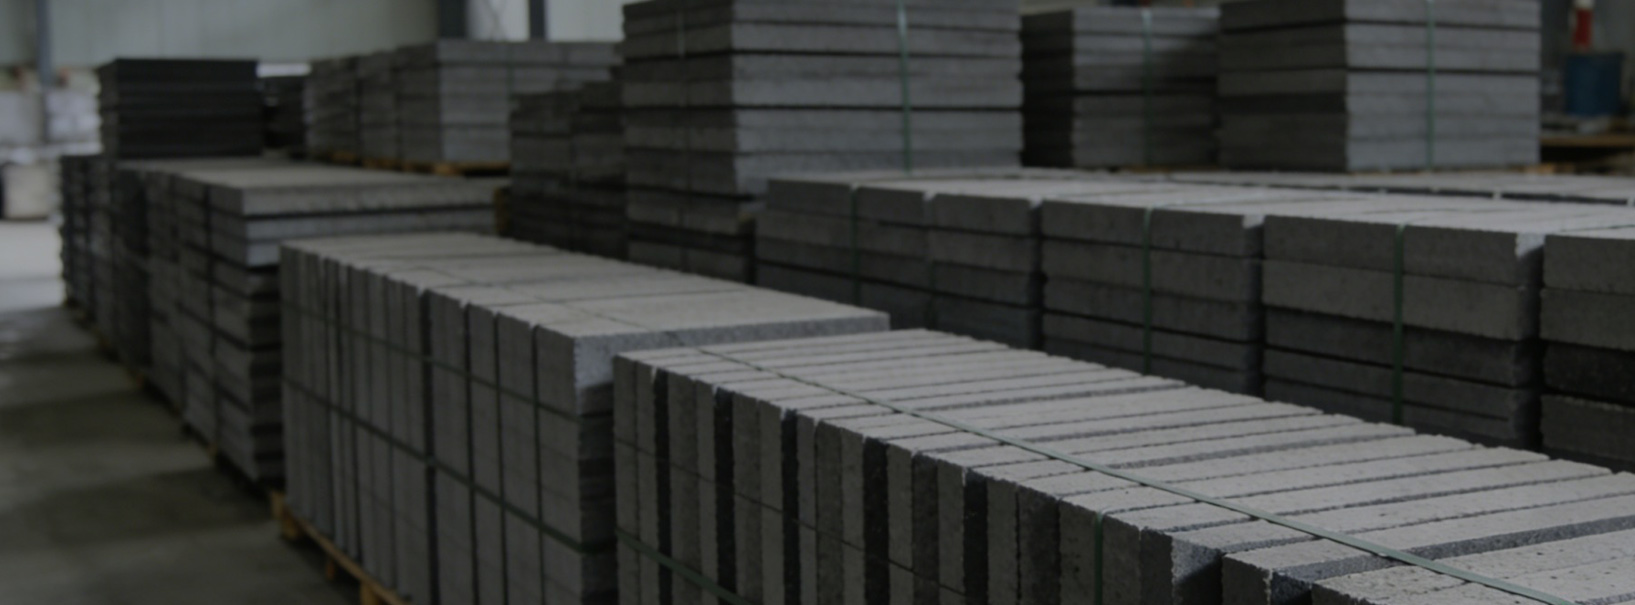
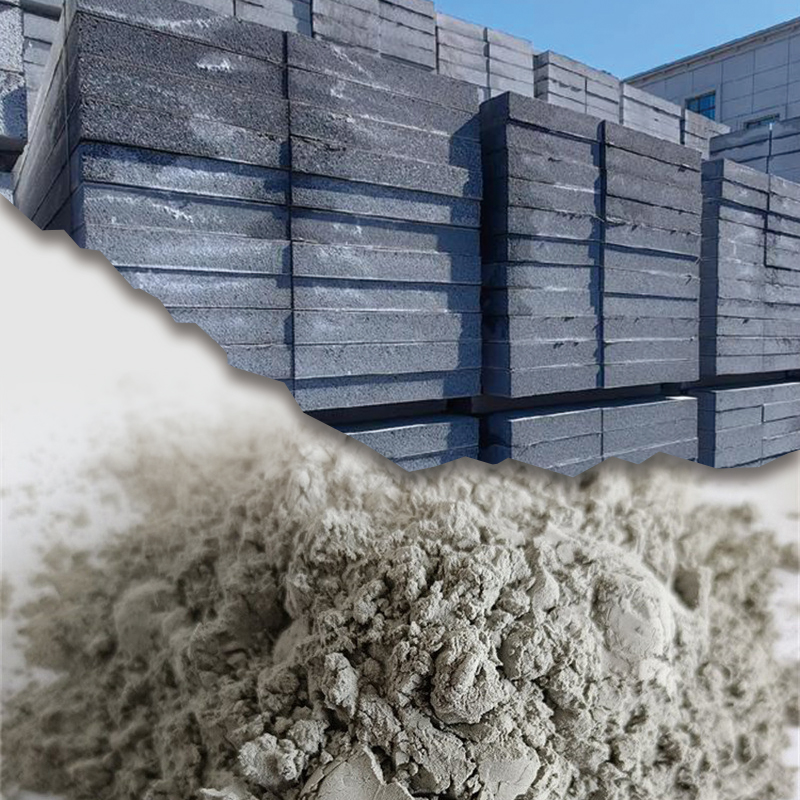
Pioneering composite integration of ultrafine mineral powders with expanded graphite, setting a new benchmark for Class-A1 fireproofing, high thermal resistance, and lightweight structural tech enclosures.
View Case Study →A granular look into how particle size distribution (PSD), specific surface area (SSA), and chemical reactivity combine to solve challenging engineering constraints in modern electronics and high-performance composites.
Standard mineral powders often leave microscopic voids within polymer or hydraulic binder systems. Our ultrafine mineral powders (with D50 values tightly centered at 14.73μm and custom grades under 5μm) physically interlock between coarser aggregates or polymer chains. This micro-filling effect minimizes capillary porosity, reduces water/moisture permeability by up to 65%, and densifies the Interfacial Transition Zone (ITZ). In electronic circuit encapsulation and technical coatings, this directly translates into ultra-high barrier protection against ionic migration and corrosive moisture penetration.
Featuring high glassy amorphous SiO&sub2; and Al&sub2;O&sub3; components, our ultrafine GGBFS and fly ash blends chemically react with free calcium hydroxide [Ca(OH)&sub2;] released during hydration. This secondary pozzolanic reaction generates dense Calcium Silicate Hydrate (C-S-H) gels and Calcium Aluminate Hydrate (C-A-H) networks, creating exceptional long-term mechanical strength, chemical abrasion resistance, and sulfate resistance in severe operational environments.
For electronic and tech composite applications, particle surfaces can be tailored to ensure optimal organophilicity and wet dispersion. Through advanced milling and surface modification techniques, our mineral powders exhibit superior compatibility with epoxy resins, polyurethanes, silicones, and phenolic polymers. This prevents agglomeration, maintains low melt viscosity during injection molding, and prevents dielectric breakdown under high voltage gradients.
When utilized in fireproof insulation boards, data center structural enclosures, and battery module potting compounds, ultrafine mineral matrices act as effective thermal sinks and smoke suppressants. The high crystalline density disperses concentrated heat spots, while the inorganic composition ensures zero volatile organic compound (VOC) emissions and non-combustible Class-A1 fire protection.
With industrial manufacturing heritage roots dating back to 1958, our processing lines maintain strict adherence to international quality management systems, rigorous testing protocols, and complete trace-to-source batch control.
Decades of continuous material refinement, research investments, and modern ball-mill engineering.
Our laboratories employ laser diffraction particle size analyzers, X-ray fluorescence (XRF) spectrometers, and automated compressive strength test benches to ensure zero-defect material shipments.
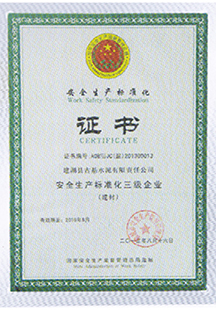
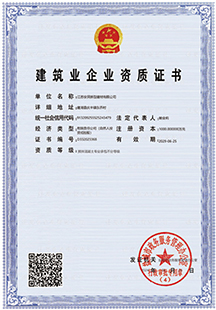
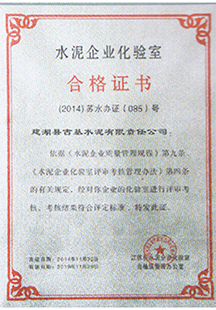
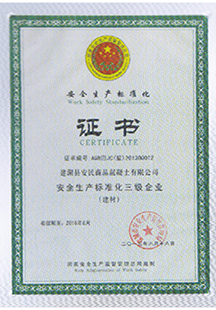
IATF 16949, CE, FMEA, PPAP, APQP, SPC AND MSA 100% TESTED
Every batch of wholesale ultrafine mineral powder undergoes complete Advanced Product Quality Planning (APQP) and Statistical Process Control (SPC) monitoring, ensuring absolute batch consistency for domestic and global export partners.
Stay informed with our latest research papers, industrial trial reports, and breakthroughs in green cementitious powder technology.
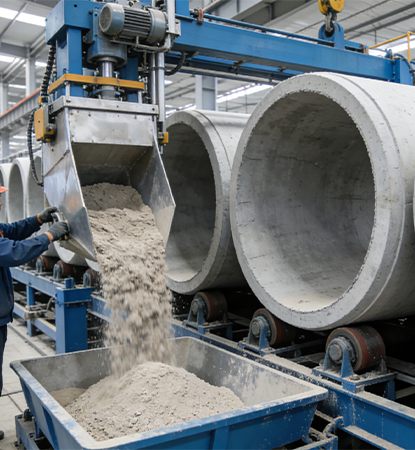
Detailed technical review of how incorporating ultrafine GGBFS composite admixtures enhances early de-molding strength, eliminates surface pore defects, and reduces steam curing cycles by up to 25%.
Read Full Analysis →
Our proprietary solid-waste mineral upcycling project successfully passes high-level technical evaluations, delivering sustainable, high-reactivity mineral binders for eco-conscious developers.
Read Full Analysis →
Comprehensive national quality testing confirms 100% compliance across all particle distribution metrics, Blaine fineness indices, and compressive activity indices for high-performance building materials.
Read Full Analysis →Browse our complete line of ultrafine mineral powders, specialized cement replacements, and custom chemical admixtures engineered for global wholesale procurement.
Premium micronized powder with exceptional micro-filler efficiency and high pozzolanic reactivity.
Standardized masonry binder offering smooth workability, stable setting, and consistent bonding power.
High-grade structural composite cement tailored for demanding engineering specifications and durability.
Engineered dual-component micro-powder delivering enhanced compressive strength and low permeability.
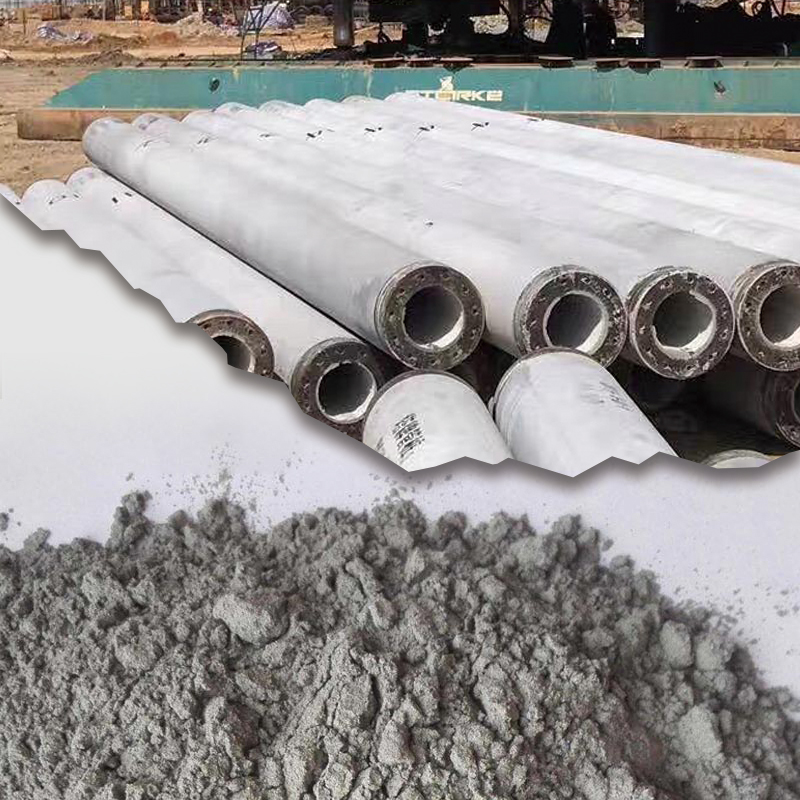
Specialized additive formulated for high-speed centrifugal precast concrete pipe piles and poles.
Inorganic thermal barrier additive engineered for graphite-modified and cement-based fireproof boards.
High-efficiency clinker replacement powder enabling substantial raw material cost savings.
Precision-milled mineral powder with guaranteed D50 granulometry for ultra-dense composite formulations.
Also explore our specialized grades: Ready-Mix Concrete Ultrafine Admixture • General Construction Grade Ultrafine Mineral Powder
View Complete Product CatalogEssential information for material engineers, procurement managers, and R&D formulators regarding particle sizing, packaging, global logistics, and custom formulation blending.
Our standard high-reactivity lines feature a D50 median diameter of 14.73μm with a 45μm sieve residue of less than 0.5%. For specialized tech composite and electronic encapsulation requirements, our dual ball-mill systems (φ3.2*13m and φ2.6*13m) equipped with high-efficiency air classifiers can deliver customized ultrafine fractions down to D50 ≤ 5.0μm with strict cut-off control against oversize grains.
By replacing 20% to 35% of expensive virgin resins, high-cost cement clinker, or synthetic fillers with our cost-saving mineral powder (such as the 30% Dosage Economic Ultrafine Powder), manufacturers significantly reduce bill-of-materials costs. Simultaneously, the micro-packing effect improves matrix density, eliminates micro-voids, enhances surface smoothness, and reduces shrinkage cracking.
We provide versatile packaging tailored to international transit and automated silo discharge: 25kg multi-wall moisture-proof craft paper bags, 1.0–1.2 metric ton UV-resistant jumbo FIBC bags with bottom discharge spouts, and bulk pneumatic tanker deliveries for regional commercial concrete and manufacturing facilities.
Operating under strict IATF 16949, CE, and ISO protocols, every batch is monitored via real-time online sampling, automated Blaine fineness meters, and laser particle analysis. Full PPAP/APQP documentation and Certificates of Analysis (COA) detailing moisture (<0.5%), loss on ignition (LOI), and 7-day/28-day activity indices accompany all international and domestic shipments.
 Send
Email
 Phone
